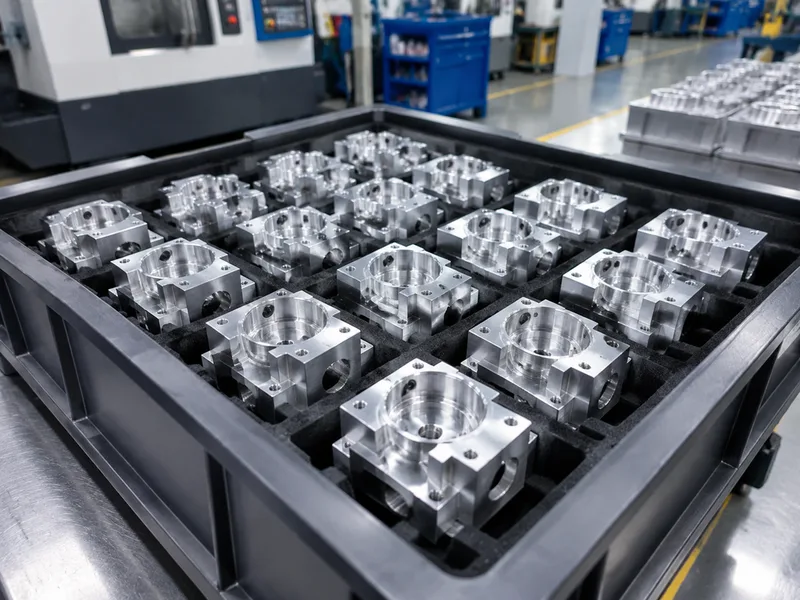
အနည်းအရေအတွက် CNC ထုတ်လုပ်မှုသည် pilot အသုတ်များ၊ စျေးကွက် စမ်းသပ်မှု အသုတ်များ၊ အစားထိုး အစိတ်အပိုင်းများနှင့် ကိရိယာ ထုတ်လုပ်ရေးကို လွှမ်းခြုံ၍ — ပုံမှန်အားဖြင့် ဆယ်ခုမှ ထောင်ပေါင်းများစွာအထိ။ အစိတ်အပိုင်းများကို စက်တင်သဖြင့် ပုံသွင်းကိရိယာ သို့မဟုတ် ကိရိယာ ရင်းနှီးမြှုပ်နှံမှု မလိုဘဲ အသုတ်ကြား ဒီဇိုင်း ပြောင်းလဲမှုများကို ကုန်ကျစရိတ် မလိုဘဲ ပြုလုပ်နိုင်သည်။
အမှာစာတစ်ခုစီကို လိုင်းတည်းနှင့် setup တည်းပေါ်တွင် ထားရှိ၍ ပထမနမူနာ ရလဒ်များကို စာရွက်စာတမ်းမှတ်တမ်းတင်သဖြင့် အစိတ်အပိုင်း တစ်သောင်းသည် အစိတ်အပိုင်း တစ်ခုနှင့် တူညီသည်။ အရေအတွက် ဈေးနှုန်း အသွင်ကူးပြောင်းသည့်အချက်များကို ရှေ့တွင် ဈေးနှုန်းတင်၍ ထုတ်ကုန် စီးပွားရေးကို ရိုးသားစွာ စီမံနိုင်စေသည်။
စွမ်းဆောင်ရည်များ
- ပုံမှန် အရေအတွက် 10 မှ 1,000+ အစိတ်အပိုင်းများ
- ကိရိယာ သို့မဟုတ် ပုံသွင်းကိရိယာ ရင်းနှီးမြှုပ်နှံမှု မလို
- အမှာစာအသုတ်တစ်ခုစီအတွက် လိုင်းတည်းနှင့် စာရွက်စာတမ်းပါ settings
- လည်ပတ်မှုတိုင်းတွင် ပထမနမူနာနှင့် နောက်ဆုံး စစ်ဆေးမှု
- အရေအတွက် ဈေးနှုန်း အသွင်ကူးပြောင်းသည့်အချက်များကို ရှေ့တွင် ဈေးနှုန်းတင်သည်
အသုံးများသော ကုန်ကြမ်းများ
အလူမီနီယမ် သတ္တုစပ်များ၊ စတိန်းလက်စ်သံမဏိ၊ ကာဗွန် သံမဏိ၊ ကြေးဝါ၊ ကြေးနီနှင့် အင်ဂျင်နီယာ ပလပ်စတစ်များ — ပရိုတိုတိုက်ပ်များအတွက် အသုံးပြုသည့် အဆင့်များကိုသာ အသုံးပြု၍ အတည်ပြုမှု ဆက်လက်ရှိသည်။
| ကုန်ကြမ်း / အဆင့် | ပုံမှန် အခြေအနေ | စက်တင်နိုင်မှု | လိုက်ညီသော အသုံးချမှု |
|---|---|---|---|
| Aluminium 6061 | T6 (solution treated and aged) | လွယ်ကူ: စက်တင်ရလွယ်၊ chips ထိန်းချုပ်မှုကောင်း | ဘရက်ကတ်၊ ဟော်ဇင်း၊ fixture များ၊ ပရိုတိုတိုက်ပ်မှ ထုတ်လုပ်မှုအထိ |
| Aluminium 7075 | T6 / T651 | ပိုခက်: ကိရိယာ ပွန်းစားမှု ပိုများ၊ တည်ငြိမ်သော setup များ လိုအပ် | ခွန်အားမြင့်၊ အလေးချိန်အရေးပါသော အစိတ်အပိုင်းများ; ချိတ်ဆက်ခြင်းအတွက် မသင့် |
| Stainless 304 / 304L | Annealed | Work-hardens: ပိုနှေးသော အမြန်များ၊ positive feed | အထွေထွေ ချေးတက်မှုခံနိုင်ရည်၊ အစားအသောက်နှင့် လုပ်ငန်းစဉ် ကိရိယာများ |
| Stainless 316 / 316L | Annealed | 304 ထက် ပိုမာ: ကိရိယာ ပွန်းစားမှု ပိုများ | Chloride၊ ပင်လယ်၊ ဆေးဘက်ဆိုင်ရာနှင့် ဆေးဝါး ထိတွေ့မှုများ |
| Carbon steel 1018 / 1045 | As-rolled / normalised | လွယ်မှ အလယ်အလတ်; ချေးတက်မှုမှ ကာကွယ်မှု လိုအပ် | ဝင်ရိုးတန်းများ၊ ပြားများ၊ ချိတ်ဆက်တည်ဆောက်ပုံများ၊ ကိရိယာ ကိုယ်ထည်များ |
| Brass C360 | H02 half hard | ထူးခြားစွာကောင်း: အမြန်များမြင့်၊ မျက်နှာပြင် သန့်ရှင်း | ချိတ်ဆက်ကိရိယာများ၊ ဘူရှင်များ၊ ချိတ်ဆက်ပိုင်းများ၊ အလှအပ အစိတ်အပိုင်းများ |
| Copper C110 | Annealed / H02 | ချောင်းစေး: ထက်မြသော ကိရိယာများနှင့် rake ထောင့်မြင့် | လျှပ်စစ်စီးကူးမှု၊ busbar များ၊ အပူစီမံခန့်ခွဲမှု |
| Titanium Grade 5 (Ti-6Al-4V) | Mill annealed | ခက်ခဲ: နှေးသော အမြန်များ၊ အပူထိန်းချုပ်မှု၊ ကိရိယာ ပွန်းစားမှု | လေကြောင်း၊ ဆေးဘက်ဆိုင်ရာနှင့် အလေးချိန်နည်း ခွန်အားမြင့် အစိတ်အပိုင်းများ |
| Engineering plastics (POM, PEEK, PA) | Extruded / annealed | လွယ်မှ ချောင်းစေး: ပျော့သော jaw များ၊ ထက်မြသော ကိရိယာများ | လျှပ်ကာ၊ ပွတ်တိုက်မှုနည်း၊ ဓာတုနှင့် ပွန်းစားမှု အစိတ်အပိုင်းများ |
မျက်နှာပြင် အလှဆင်မှုများ
အလှဆင်မှု အကျယ်အဝန်း အပြည့်အစုံ - အန်နိုဒိုင်ဇင်း၊ သတ္တုကပ်ခြင်း၊ ပါဝါကိုတင်း၊ ပက်စီဗေးရှင်း၊ ပွတ်သပ်အလင်းပြန်ခြင်းနှင့် အမှတ်အသား၊ အသုတ်များကြား တစ်သမတ်တည်း အသုံးချသည်။
| အလှဆင်မှု | မည်သို့အကျိုးပြုသည် | မည်သည့်အခါ သတ်မှတ်သင့်သည် |
|---|---|---|
| စက်တင်အတိုင်း | ကိရိယာ အမှတ်အသားများ မြင်နေနိုင်; Ra ပုံမှန်အားဖြင့် 1.6-3.2 µm | အစိတ်အပိုင်းသည် လုပ်ဆောင်နိုင်ရုံသာ လိုအပ်လျှင် |
| Bead blast | တစ်သမတ်တည်း matte မျက်နှာပြင်၊ ကိရိယာ အမှတ်အသားများ ဖုံးကွယ် | အန်နိုဒိုင်ဇင်းမပြုလုပ်မီ အလှအပ အစိတ်အပိုင်းများ |
| အန်နိုဒိုင်ဇင်း Type II | အောက်ဆိုက် လွှာ တည်ဆောက်သည်; အရောင် ရွေးချယ်စရာများ | Aluminium အသွင်အပြင်နှင့်အတူ အလယ်အလတ် ချေးတက်နှင့် ပွန်းစားမှု ခံနိုင်ရည် |
| Hard အန်နိုဒိုင်ဇင်း Type III | ပိုထူပြီး ပိုမာသော အောက်ဆိုက် လွှာ | ပွတ်တိုက်သော သို့မဟုတ် ပွန်းစားသော aluminium မျက်နှာပြင်များ |
| Chromate conversion | လျှပ်စစ်စီးကူးမှု ဆက်လက်ရှိသော ပါးလွှာသည့် ကာကွယ်လွှာ | Aluminium ပေါ်တွင် လျှပ်စစ် bonding သို့မဟုတ် grounding |
| Electroless nickel | တစ်သမတ်တည်း၊ မာပြီး ချေးတက်မှုခံနိုင်သော လွှာ | ပွန်းစားမှုနှင့် ချေးတက်မှု၊ bore အတွင်းပိုင်းများ အပါအဝင် |
| Zinc plating | စီးပွားရေး အကျိုးရှိသော ချေးတက်မှု ကာကွယ်မှု | အိမ်တွင်း သို့မဟုတ် အမိုးအကာရှိ သံပြား အစိတ်အပိုင်းများ |
| Powder coat | ထူပြီး ခံနိုင်ရည်ရှိ အလှအပ လွှာ | အသွင်အပြင်ကိုယ်တိုင် လိုအပ်ချက်ဖြစ်လျှင် |
| Passivation | ကိုယ်ပိုင် သံမာများ ဖယ်ရှား၍ အောက်ဆိုက် လွှာ ပြန်လည်ထူထောင် | စက်တင်ပြီးသော စတိန်းလက်စ်သံမဏိ အစိတ်အပိုင်းများ |
| Stress relief / heat treatment | ဖြတ်တောက်မှု မတိုင်မီ သို့မဟုတ် နောက်တွင် ကျန်ရှိတင်းအားများ ပြန်လည်လျှော့ချ | စက်တင်ခြင်းကို ခံနိုင်ရန် လိုအပ်သော ပါးလွှာသော နှုတ်ခမ်းများနှင့် ကျပ်ကျပ်စည်းစည်း ခွင့်ပြုချက်များ |
ခွင့်ပြုချက်များ
ပုံမှန် ISO 2768-m; ထပ်ခါထပ်ခါ အမှာစာများသည် ပထမနမူနာပေါ်တွင် အတည်ပြုထားသော ခွင့်ပြုချက်များကို ထိန်းသိမ်းသည်။
| ဆွဲပုံတောင်းဆိုချက် | မည်သည့်အရာ လိုအပ်သည် | ကုန်ကျစရိတ်နှင့် ပို့ဆောင်ချိန်အပေါ် သက်ရောက်မှု |
|---|---|---|
| အထွေထွေ: ±0.25 mm / ±0.010 in | ပုံမှန် ကိရိယာ၊ အတိုင်းအတာ စစ်ဆေးမှု | အခြေခံ: ပိုတိုးခ မရှိ |
| ပုံမှန်: ±0.13 mm / ±0.005 in | အခြေအနေကောင်းသော စက်၊ ပထမနမူနာ စစ်ဆေးမှု | ပိုတိုးခ အနည်းငယ်; ဈေးနှုန်းတင်ရာတွင် ပုံသေအဖြစ် အသုံးပြု |
| ကျပ်ကျပ်: ±0.025 mm / ±0.001 in | ပွတ်ချောထားသော သို့မဟုတ် စိန် ကိရိယာများ၊ အပူချိန်ထိန်းချုပ်မှု၊ CMM | အဆင့်တက်ပြောင်းမှု: ဖြတ်တောက်မှုနှေးကျွံပြီး စစ်ဆေးမှု အပြည့်အစုံ |
| တိကျမှု: ±0.013 mm / ±0.0005 in | ပြီးစီးအဆင့် ဖြတ်တောက်မှုများ၊ gauge များ၊ ထိန်းချုပ်ထားသော ပတ်ဝန်းကျင် | စက်တင်ခြင်းက ဈေးနှုန်းကို သတ်မှတ်သည်; မကြာခဏ သီးသန့် လုပ်ငန်းစဉ် |
| တည်နေရာ / ထောင့်တည်ငြိမ်မှု (GD&T) | ဒေတာထိန်းချုပ်မှု၊ အင်္ဂါရပ်များ ဆက်စပ်နေလျှင် setup တစ်ခုတည်း | ဒေတာက မည်မျှ setup ကို ဖြတ်သန်းသည်ပေါ် မူတည်သည် |
| မျက်နှာပြင် ပြီးမြောက်အဆင့် Ra 0.8 µm သို့မဟုတ် ပိုမွမ်းမံ | ပိုသေးသော stepover များ၊ ပွတ်သပ်ခြင်း သို့မဟုတ် ပြီးစီးအဆင့် ဖြတ်တောက်မှု | စက်တင်ချိန်သာမက လုပ်ငန်းစဉ် အဆင့်တစ်ခု ထပ်ပေါင်းသည် |
Pilihan Proses
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Ordering, Lead Times & MOQ
Custom CNC parts carry no forced MOQ; ordering from a single prototype piece is standard industry practice.
Instant-quote platforms publicly advertise prototype lead times of 1-3 business days.
Online RFQ is the industry-standard flow: upload a 3D model (STEP/STP/DWG/DXF), receive an instant quote or engineer review, then production, inspection, and delivery.
မေးလေ့ရှိသော မေးခွန်းများ
ထပ်ခါထပ်ခါ အမှာစာများကြား အရည်အသွေး တစ်သမတ်တည်းဖြစ်မှုကို မည်သို့ထိန်းသိမ်းပါသလဲ။
အမှာစာအသုတ်တစ်ခုစီသည် လိုင်းတည်းနှင့် setup တည်းပေါ်တွင် ရှိသည်။ ပထမနမူနာကို စစ်ဆေး၍ စာရွက်စာတမ်းမှတ်တမ်းတင်ပြီး လုပ်ငန်းစဉ်အတွင်း settings များကို မှတ်တမ်းတင်၍ လည်ပတ်မှုတိုင်းတွင် နောက်ဆုံး စစ်ဆေးမှု ထပ်လုပ်သည်။ ထပ်ခါထပ်ခါ အမှာစာများကို မူလ အတည်ပြုထားသော နမူနာနှင့် တိုက်ဆိုင်စစ်ဆေးသည်။
Injection molding ထက် အနည်းအရေအတွက် CNC ပိုကောင်းသည် မည်သည့်အခါ ဖြစ်ပါသလဲ။
ခန့်မှန်းခြေ ထောင်ပေါင်းအနည်းငယ်အောက်တွင် CNC က အနိုင်ယူသည် - ပုံသွင်းကိရိယာ ရင်းနှီးမြှုပ်နှံမှု မလို၊ ကိရိယာ ပို့ဆောင်ချိန် မလို၊ အသုတ်ကြား ဒီဇိုင်း လွတ်လပ်မှု အပြည့်အစုံ။ Injection molding သည် ပုံသွင်းကိရိယာ ကုန်ကျစရိတ် ပြန်လည်ရရှိသည့် အရေအတွက်တွင်သာ အကျိုးပြု၍ — ပလပ်စတစ်အတွက်သာ။ သင်၏ အစိတ်အပိုင်းအတွက် အသွင်ကူးပြောင်းမှု မည်သည့်နေရာတွင် ရှိသည်ကို ကျွန်ုပ်တို့ ရိုးသားစွာ ပြောပြမည်။
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 2
- rapiddirect.comIndustry peer technical page
- jlccnc.comIndustry peer technical page
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
ဆက်စပ် ဝန်ဆောင်မှုများ
Related Knowledge
Capability commitments on this page are owner-confirmed (2026-09-21).