Sinker EDM
Sinker EDM for blind cavities, mold details and complex 3D forms in hard conductive metals: tolerances to ±0.005–0.01 mm, fine finishes down to Ra 0.2–0.8 µm, no cutting forces.
Last updated: 2026-10-28
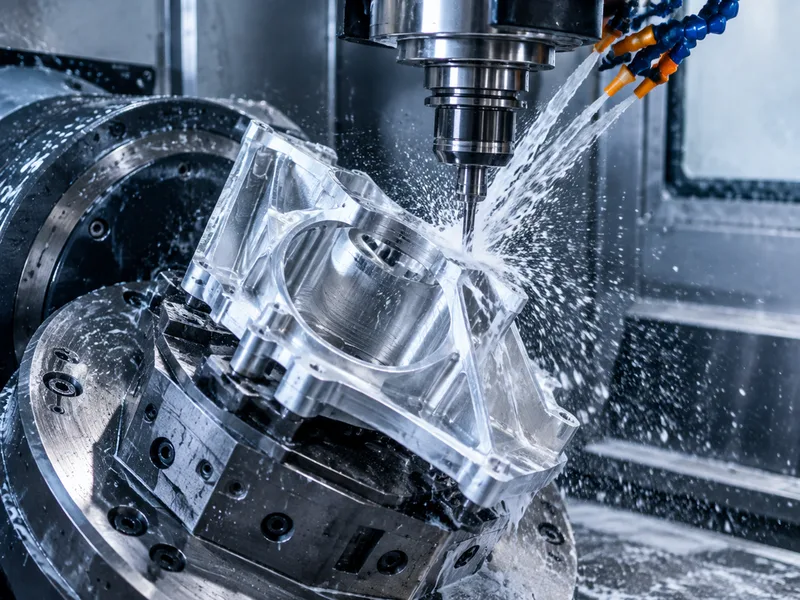
Sinker EDM (also called ram or die-sinking EDM) erodes a cavity by discharging a shaped electrode into the workpiece, one spark at a time, inside a dielectric fluid. Where wire EDM can only cut through-profiles, the electrode can sink anywhere a through-path does not exist — which makes sinker EDM the process for blind cavities, mold details, ribs and complex 3D forms.
Because the spark never touches the workpiece, no cutting force acts on the part: deep cavities and thin features hold geometry in fully hardened steel where a milling cutter would deflect. The evidence-backed capability band runs from ±0.005–0.01 mm in stable conditions down to ±0.0001 in (0.00254 mm), with finishing passes reaching Ra 0.2–0.8 µm on the characteristic matte EDM texture.
Stable setups hold ±0.005 mm to ±0.01 mm, with tolerances as low as 0.0001 in (0.00254 mm) reported through controlled spark cutting — no cutting force means no tool deflection on deep cavities and thin features. Electrode count is the main cost lever: simple cavities run on one or two electrodes, while complex molds need a full roughing, semi-finishing and finishing electrode set.
Specifications
| Specification | Sinker EDM |
|---|---|
| Tolerance | ±0.005–0.01 mm stable conditions; down to ±0.0001 in (0.00254 mm) |
| Lead Time | EDM parts ship in 5–10 days standard; one insert for first article typically 5–10 days including electrode manufacture; multi-cavity programs 12–25 days |
Materials
Surface Finishes
Sinker (ram) EDM burns a custom-shaped electrode into conductive workpieces to produce blind cavities, mold details and complex 3D forms that through-cutting wire EDM cannot reach. No cutting forces act on the part, so deep cavities and thin features hold geometry in hardened steel, tungsten and carbide. Catalog tolerance evidence runs from ±0.005–0.01 mm in stable conditions down to ±0.0001 in (0.00254 mm); finishing passes reach Ra 0.2–0.8 µm on the characteristic matte EDM texture.
Values above are the collected catalog specification envelope for this product family. Tolerances and lead times at the demanding end of a range are confirmed for the specific geometry, material and batch at quotation.
Applications & Selection Points
Blind cavities and mold details
The defining sinker job: a closed pocket with no wire exit — mold cores, cavity details, embossing dies. The electrode is manufactured in the shape of the cavity, so geometry freedom is high but each cavity shape needs its own electrode; complex cavities are often roughed with a low-cost electrode and finished with a precision one.
Hardened and exotic conductive metals
Sinker EDM cuts at full hardness: hardened tool steel, tungsten and carbide are routine, and any electrically conductive metal is feasible. Parts go to EDM after heat treatment, so there is no anneal-remachine-reharden cycle and no distortion from cutting forces.
Deep, thin and delicate features
Thin ribs, deep narrow slots and fine detail edges survive sinking because nothing pushes on them. Accuracy comes from controlling the spark gap, electrode geometry and burn parameters rather than mechanical rigidity — state the deepest and thinnest features explicitly when requesting a quote.
Finish-critical surfaces
Each discharge leaves a microscopic crater; roughing passes leave a coarse matte texture and finishing passes with lower energy refine it down the Ra band. Spec the finish on functional surfaces only — carrying the finest finish across the whole cavity multiplies electrode passes and cost.
Frequently Asked Questions
Sinker EDM vs wire EDM — which process does my part need?
Wire EDM cuts through-geometry: the electrode is a stretched wire, so the result is always a pierced profile. Sinker EDM burns a shaped cavity into the surface, so it is the only EDM answer for blind cavities, closed pockets and 3D mold details. If the feature passes through the part, wire is usually faster and cheaper; if it stops inside the material, sinker is the route.
What tolerance and surface finish can sinker EDM hold?
The collected evidence band runs from ±0.005–0.01 mm in stable conditions, with fine work quoted to ±0.0001 in (0.00254 mm). Finish improves with low-energy finishing passes down to Ra 0.2–0.8 µm. Tolerance and finish interact: each finishing pass removes recast and improves finish at added cycle time, so specify both only where the part function requires them.
What does a sinker EDM quote need?
A 3D model or sectioned drawing of the cavity, the material and its hardness state, depth and corner radii, tolerance and finish on functional surfaces, and quantity. Electrode fabrication is part of the cost — mention whether you can supply an electrode design or need one engineered from the model. Confirm material conductivity, the feasibility gate for the whole process, at quotation.
Ordering & Documentation
Documents
A 3D model (STEP preferred) or a dimensioned section drawing showing cavity depth, corner radii and the tolerance/finish callouts on functional surfaces. State the heat-treat condition of the incoming material — burn strategy changes with hardness.
Quotation
Pricing inputs: cavity volume and depth (burn time scales with removed volume), electrode count and complexity, finish spec (each finishing pass adds cycle time), material, quantity and destination. Quotes where no finish is specified assume a standard roughing-plus-one-finish sequence and say so.
Sample & Supply
A first-article cavity burn in the production material and hardness validates spark gap and finish before a mold set is committed. Small tooling batches and single cavity repairs are the normal order shape; confirm batch pricing at quotation.
Storage & Shipping
Sunk cavities have no burrs but the recast layer is hard and edges are sharp — pack parts so cavities cannot strike each other. Keep electrode and workpiece pairs together in storage; re-matching a worn electrode to its cavity later costs a re-burn.