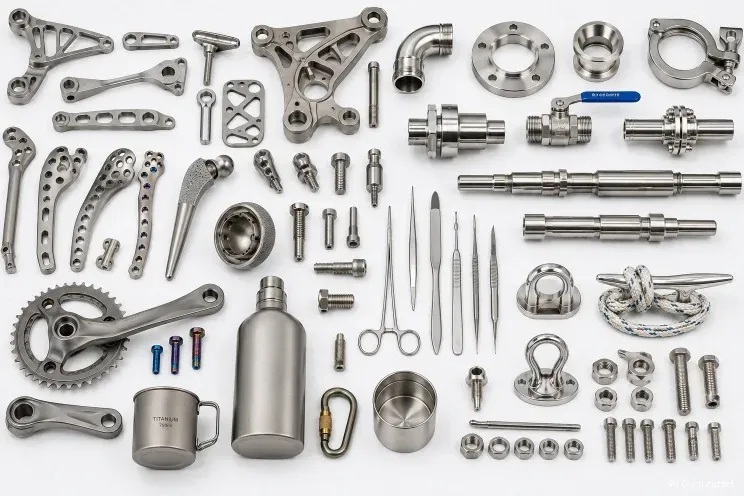
Titaniumbewerking beloont ervaring: lage thermische geleidbaarheid, versterking door vervorming en terugvering straffen verkeerde gereedschapspaden af. Wij bewerken Ti-6Al-4V (Grade 5) en commercieel zuivere Grade 2-onderdelen met stijve opspanningen en gedisciplineerd warmtebeheer.
Typische titaniumprojecten omvatten lichte constructiebeugels, sterk corrosiebelaste vloeistofcomponenten en biocompatibele onderdelen waar materiaalcertificaten en traceerbaarheid ertoe doen.
Belangrijkste specificaties
| Specification | Value |
|---|---|
| surface finish | AMS-2488 Type 2 |
| lead time | 1-2 weeks |
| tolerance | ±0.002 in |
Material Grades & Properties
Titanium Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| Grade 2 | ASTM B265 | Commercially pure; best formability/corrosion resistance; chemical and medical. |
| Grade 5 (Ti-6Al-4V) | ASTM B265 | Workhorse aerospace alloy; high strength-to-weight; most common machined titanium. |
Key Properties of Machined Titanium
- ✓Highest strength-to-weight of common metals
- ✓Extreme corrosion resistance
- ✓Biocompatible
- ✓Heat resistant
Typical tolerances:±0.05 mm standard; stress-relief consideration for thin parts
Applications for Titanium Parts
- Aerospace structural parts and fasteners
- Medical implants and surgical instruments
- Marine components
- High-performance automotive
- Sporting goods
Machining Notes for Titanium
Low thermal conductivity causes heat concentration at tool edge: low cutting speeds, high feed pressure, flood coolant, sharp carbide, never let tool dwell. Fire risk with fine chips — proper chip handling required.
Finishes for Titanium Parts
- Anodizing (color, type II/III limits)
- Passivation
- Bead blasting
Capaciteiten
- Bewerking van Ti-6Al-4V Grade 5 en CP Grade 2
- Strategieën met lage snijsnelheid en hogedrukkoelvloeistof
- Materiaaltraceerbaarheid en materiaalcertificaten
- Kenmerken met strakke toleranties na beoordeling
Typische materialen
Titanium Grade 5 (Ti-6Al-4V), Grade 2 CP, Grade 4 op aanvraag.
| Materiaal / kwaliteit | Typische toestand | Verspaanbaarheid | Waar het past |
|---|---|---|---|
| Aluminium 6061 | T6 (opgelost en uitgehard) | Makkelijk: goed verspaanbaar, goede spaancontrole | Beugels, behuizingen, opspanmiddelen, prototypen richting serie |
| Aluminium 7075 | T6 / T651 | Moeilijker: meer gereedschapsslijtage, starre opspanning nodig | Hogesterkte, gewichtskritische onderdelen; niet lasbaar |
| Stainless 304 / 304L | Zachtgegloeid | Verhardt koud: lagere snelheden, positieve voeding | Algemene corrosiebestendigheid, voedings- en procestechniek |
| Stainless 316 / 316L | Zachtgegloeid | Taaiër dan 304: meer gereedschapsslijtage | Chloriden, maritiem, medische en farmaceutische omgeving |
| Carbon steel 1018 / 1045 | gewalst / genormaliseerd | Makkelijk tot gemiddeld; heeft roestbescherming nodig | Assen, platen, lasconstructies, gereedschapslichamen |
| Brass C360 | H02 halfhard | Uitstekend: hoge snelheden, mooie afwerking | Fittingen, busjes, connectoren, decoratieve onderdelen |
| Copper C110 | Zachtgegloeid / H02 | Kleverig: scherpe gereedschappen en grote spaanhoeken | Geleidbaarheid, collectoren, warmtebeheersing |
| Titanium Grade 5 (Ti-6Al-4V) | Fabrieksgegloeid | Moeilijk: lage snelheden, warmtebeheersing, gereedschapsslijtage | Lucht- en ruimtevaart, medische techniek, lichte hogesterkte onderdelen |
| Technische kunststoffen (POM, PEEK, PA) | Geëxtrudeerd / gegloeid | Makkelijk tot kleverig: zachte klemmen, scherpe gereedschappen | Isolatie, lage wrijving, chemie- en slijtdelen |
Afwerkingen
Zoals bewerkt, passivering, anodiseren (Type II gekleurd), kogelstralen, polijsten.
| Afwerking | Wat het doet | Specificeren wanneer |
|---|---|---|
| Verspaand gelaten | Gereedschapssporen zichtbaar; Ra typisch 1.6-3.2 µm | Het onderdeel hoeft alleen te functioneren |
| Glasparelstralen | Egaal mat oppervlak, verbergt gereedschapssporen | Cosmetische onderdelen vóór anodiseren |
| Anodiseren Type II | Bouwt een oxidelaag op; kleuropties | Aluminium-uitstraling plus matige corrosie- en slijtvastheid |
| Hardanodiseren Type III | Dikkere, hardere oxidelaag | Glijdende of slijtende aluminiumoppervlakken |
| Chromatering | Dunne beschermende laag die geleidend blijft | Elektrisch verbinden of aarden op aluminium |
| Chemisch nikkel | Egaal, harde, corrosiebestendige laag | Slijtage plus corrosie, ook in boringen |
| Verzinken | Economische offerbescherming tegen corrosie | Stalen onderdelen binnen of onder een afdak |
| Poedercoaten | Dikke, duurzame, decoratieve laag | Uiterlijk is de eis |
| Passiveren | Verwijdert vrij ijzer en herstelt de oxidelaag | RVS-onderdelen na de verspaning |
| Spanningsarm gloeien / warmtebehandeling | Neemt restspanningen weg voor of na de bewerking | Dunne wanden en strakke toleranties die de bewerking moeten doorstaan |
Toleranties
±0.01 mm typisch op kritische kenmerken; CMM-verificatie op aanvraag.
| Tekenaanduiding | Wat het vereist | Effect op kosten en doorlooptijd |
|---|---|---|
| Algemeen: ±0.25 mm / ±0.010 in | Standaardgereedschap, maatcontrole | Basis: geen toeslag |
| Standaard: ±0.13 mm / ±0.005 in | Machine in goede staat, eerste-artikelcontrole | Kleine toeslag; de gebruikelijke calculatienorm |
| Strak: ±0.025 mm / ±0.001 in | Geslepen of diamantgereedschap, temperatuurbeheersing, CMM | Sprong: tragere passes plus volledige inspectie |
| Precisie: ±0.013 mm / ±0.0005 in | Finishing-passes, maten, gecontroleerde omgeving | De verspaning bepaalt de prijs; vaak een aparte bewerking |
| Positie / hoekigheid (GD&T) | Datumbeheersing, één opspanning bij samenhangende features | Hangt af van over hoeveel opspanningen de datum loopt |
| Oppervlakteruwheid Ra 0.8 µm of fijner | Fijnere instelmaten, polijsten of een afwerkpass | Voegt een processtap toe, niet alleen verspaningstijd |
Materials We Machine
- Brass
- Copper
- Grade 5
- Titanium
Common Applications
- Continuous Seawater Immersion
- Ferric Chloride
- Golf Clubs
- Medical Implants
- Racing Applications
- Structural Elements
- Wet Chlorine
- chloride-rich environments
- high-performance engineering parts
- permanent implants
- seawater
- turbine blades
- Aerospace
- Automotive
- Medical
Procesopties
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Veelgestelde vragen
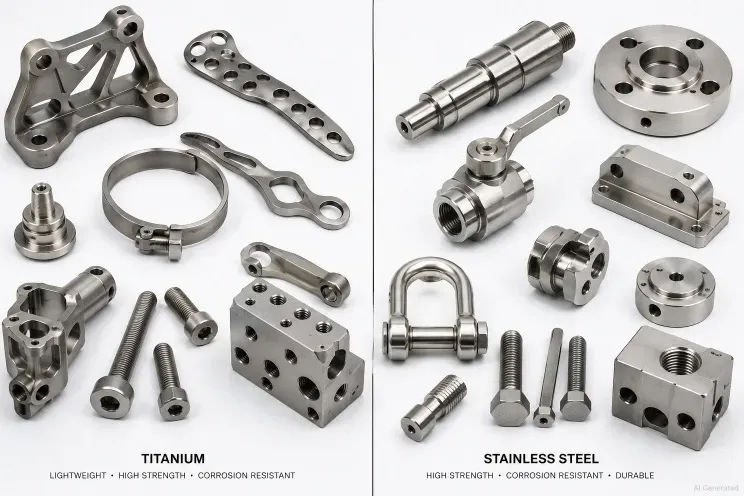
Is titanium het waard vergeleken met roestvast staal?
Wanneer sterkte-gewicht, corrosiebestendigheid of biocompatibiliteit het ontwerp bepaalt, wint titanium ondanks de hogere kosten. Voor statische, prijsgedreven onderdelen is roestvast staal doorgaans voldoende.
Kunt u titanium materiaalcertificaten leveren?
Ja. Materiaalcertificaten met chemische samenstelling en mechanische eigenschappen worden met de zending meegeleverd.
Hoe houdt u de kosten van titaniumbewerking laag?
Door het proces vroeg vast te leggen: juiste wisselplaten, stabiele uitsteeklengtes, hogedrukkoelvloeistof en DFM-feedback die onnodig strakke toleranties verwijdert.
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- ecoreprap.comUnclassified source
- fictiv.comIndustry peer technical page
- rapiddirect.comIndustry peer technical page
- facturee.deUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Gerelateerde diensten
Capability commitments on this page are owner-confirmed (2026-09-21).