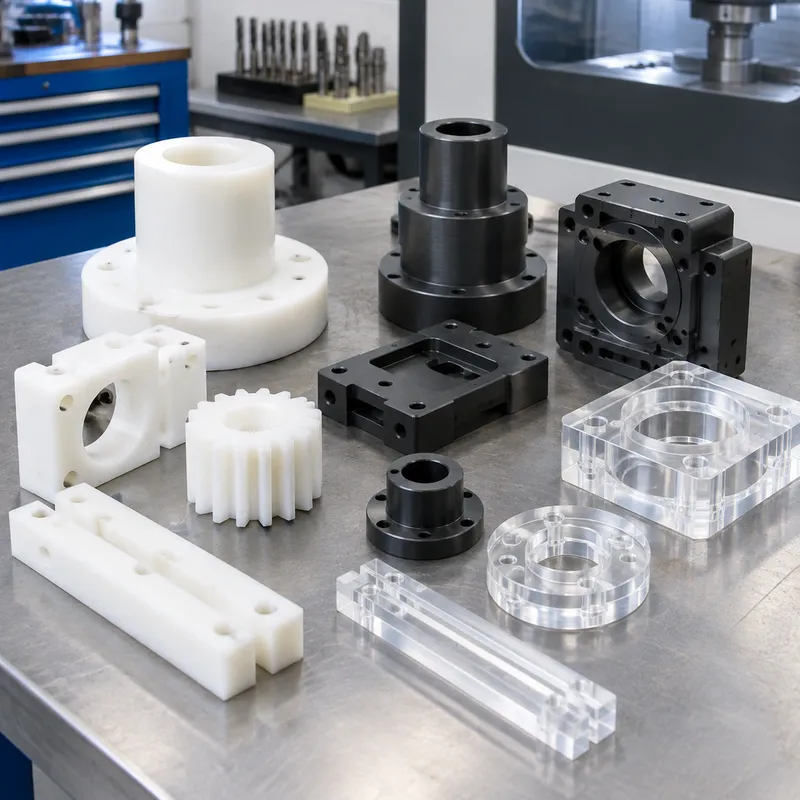
我們加工的塑膠零件涵蓋試作品、絕緣件、齒輪、襯套、耐磨零組件、醫療級 PEEK 零件與光學壓克力鏡片:一般用途用 ABS 與 POM(Delrin)、耐磨用尼龍 6/6、耐溫與滅菌用 PEEK、耐化學與低摩擦用 PTFE。
塑膠的加工方式與金屬不同——熱膨脹約為金屬的十倍且熱量累積很快,因此我們採用銳利的研磨刀具、保守的轉速與順銑,避免邊緣熔融或崩裂。公差反映材料的真實能力,而非一廂情願。
Material Grades & Properties
Engineering Plastics Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| POM (Delrin/Acetal) | — | Low friction, high stiffness, dimensional stability; gears, bushings, precision parts. |
| Nylon (PA6/PA66) | — | Tough and wear-resistant; absorbs moisture (dimension planning needed). |
| PEEK | — | High-performance: chemical/heat resistance; medical implants, aerospace; expensive. |
| ABS | — | Impact resistant, low cost; prototyping and housings. |
| PTFE (Teflon) | — | Near-zero friction, chemical inertness; seals and insulators; hard to hold tolerance. |
Key Properties of Machined Engineering Plastics
- ✓Light weight
- ✓Corrosion-free
- ✓Low friction options
- ✓Electrical insulation
Typical tolerances:±0.1 mm typical; thermal expansion and moisture limit precision
Applications for Engineering Plastics Parts
- Gears and bushings
- Insulators
- Seals and wear strips
- Medical device components (PEEK)
- Enclosures and jigs
Machining Notes for Engineering Plastics
Sharp positive-rake tools, moderate speeds, air blast or coolant; watch heat buildup (melting) and clamping pressure (deformation).
Finishes for Engineering Plastics Parts
- As-machined (typical)
- Vapor polishing (select plastics)
- Dyeing
加工能力
- ABS/POM/尼龍/PEEK/PTFE 依圖面加工
- 對抗熔融與崩裂的銳利刀具策略
- 壓克力火焰與布輪拋光
- 應力消除退火協調
常用材料
ABS、POM-C(Delrin)、尼龍 6/6、PEEK、PTFE、HDPE/UHMW、聚碳酸酯、壓克力(PMMA)。
| 材料 / 牌號 | 常見交貨狀態 | 切削性 | 適用情境 |
|---|---|---|---|
| 鋁合金 6061 | T6(固溶處理及時效) | 容易:切削性佳,切屑控制良好 | 支架、機殼、治具,從試作品到進入量產 |
| 鋁合金 7075 | T6 / T651 | 較難:刀具磨耗較大,需要剛性設定 | 高強度、重量敏感零件;不適合焊接 |
| 不鏽鋼 304 / 304L | 退火 | 加工硬化:轉速較低、正前角進給 | 一般耐腐蝕,食品與製程設備 |
| 不鏽鋼 316 / 316L | 退火 | 較304更韌:刀具磨耗更大 | 氯化物、船舶、醫療與製藥環境 |
| 碳鋼 1018 / 1045 | 軋延態 / 正常化 | 容易至中等;需防鏽保護 | 軸件、板件、焊接組裝件、工裝本體 |
| 黃銅 C360 | H02 半硬 | 極佳:高轉速、表面潔淨 | 接頭、襯套、連接器、裝飾零件 |
| 銅 C110 | 退火 / H02 | 黏性強:需銳利刀具與大前角 | 導電、匯流排、熱管理 |
| 鈦 Grade 5 (Ti-6Al-4V) | 出廠退火(mill annealed) | 困難:低轉速、熱控制、刀具磨耗 | 航太、醫療與輕量化高強度零件 |
| 工程塑膠(POM、PEEK、PA) | 押出 / 退火 | 容易至黏性:軟爪、銳利刀具 | 絕緣、低摩擦、耐化學與耐磨零件 |
表面處理
原加工面、去毛邊、壓克力火焰/布輪拋光、退火依需求提供。
| 表面處理 | 作用 | 適用時機 |
|---|---|---|
| 原加工面 | 留有刀痕;Ra 通常 1.6–3.2 µm | 零件只需具備功能 |
| 珠擊處理 | 均勻霧面,遮蓋刀痕 | 陽極處理前的外觀件 |
| 陽極處理 Type II | 生成氧化膜;可選顏色 | 鋁件外觀加上溫和的耐蝕與耐磨性 |
| 硬陽極處理 Type III | 更厚、更硬的氧化膜 | 滑動或磨耗的鋁件表面 |
| 鉻酸鹽皮膜處理 | 薄型保護膜且維持導電性 | 鋁件電氣搭接或接地 |
| 化學鎳 | 均勻、堅硬、耐蝕的鍍層 | 耐磨加耐蝕,含孔內 |
| 鍍鋅 | 經濟的犧牲性防蝕保護 | 室內或有遮蔽環境的鋼件 |
| 粉體塗裝 | 厚實、耐用、裝飾性塗層 | 外觀即為要求時 |
| 鈍化處理 | 移除游離鐵並重建氧化膜 | 加工後的不鏽鋼零件 |
| 應力消除退火 / 熱處理 | 在切削前後釋放殘留應力 | 必須撐過加工的薄壁與緊公差零件 |
公差
一般 ISO 2768-m;常見 ±0.05 mm,關鍵特徵 ±0.02 mm。
| 圖面標註 | 需要什麼 | 對成本與交期的影響 |
|---|---|---|
| 一般:±0.25 mm / ±0.010 in | 標準刀具、尺寸抽檢 | 基準:不加價 |
| 標準:±0.13 mm / ±0.005 in | 機台狀況良好、首件檢查 | 小幅加價;最常見的報價預設值 |
| 緊:±0.025 mm / ±0.001 in | 研磨或鑽石刀具、溫控、三次元測量儀(CMM) | 階躍變化:切削更慢加上全數檢驗 |
| 精密:±0.013 mm / ±0.0005 in | 精修程序、量規、受控環境 | 加工主宰價格;常成為獨立工序 |
| 位置度 / 傾斜度(GD&T) | 基準控制,相關特徵一次設定完成 | 取決於基準跨多少次設定 |
| 表面粗糙度 Ra 0.8 µm 或更細 | 更細的步進、拋光或精修走刀 | 增加一個製程步驟,不只是加工時間 |
Related Processes
5-axis CNC machining
used for
CNC Milling
used for
Recycling
used for
Common Applications
- Turning
- cost-sensitive prototypes
- consumer goods
加工選項
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
常見問題
我的應用該用 PEEK 還是 Delrin?
Delrin(POM-C)以中等成本滿足精密機械零件;PEEK 則以較高價格勝任高溫、滅菌與化學暴露。我們會依操作環境給建議。
為什麼塑膠公差比金屬寬?
塑膠隨溫度與應力的膨脹和鬆弛約為金屬的十倍。±0.05 mm 是常見水準;搭配尺寸穩定的材料與受控製程,關鍵特徵可維持 ±0.02 mm。
可以加工透明壓克力零件嗎?
可以。我們以銳利刀具加工壓克力,並在幾何允許時拋光至透光——請寄送圖面並註明哪些面必須保持光學透明。
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- hubs.comIndustry peer technical page
- xometry.comIndustry peer technical page
- uneedpm.comUnclassified source
- us.arrk.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Capability commitments on this page are owner-confirmed (2026-09-21).