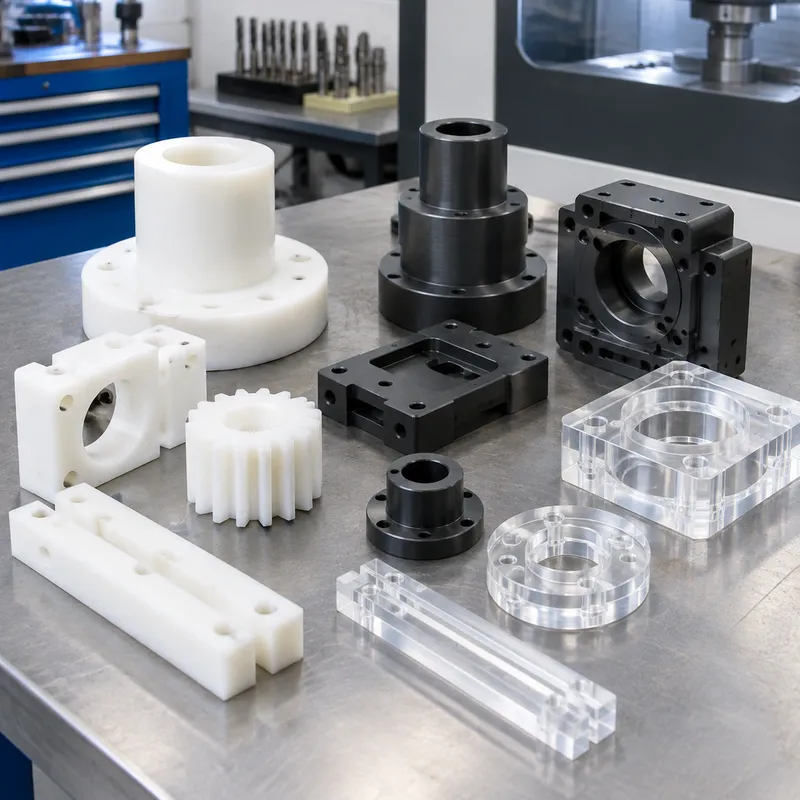
Bahagian plastik yang kami mesin meliputi prototaip, penebat, gear, bushing, komponen haus, bahagian PEEK gred perubatan dan kanta akrilik optik: ABS dan POM (Delrin) untuk kerja am, nilon 6/6 untuk haus, PEEK untuk suhu dan pensterilan, PTFE untuk kegunaan kimia dan geseran rendah.
Plastik dimesin berbeza daripada logam — pengembangan terma kira-kira sepuluh kali lebih tinggi dan haba terbina pantas, jadi kami menjalankan alat tergilap tajam, kelajuan berhati-hati dan frais sehala supaya mata alat tidak cair atau berkeping. Toleran mencerminkan bahan, bukan angan-angan.
Material Grades & Properties
Engineering Plastics Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| POM (Delrin/Acetal) | — | Low friction, high stiffness, dimensional stability; gears, bushings, precision parts. |
| Nylon (PA6/PA66) | — | Tough and wear-resistant; absorbs moisture (dimension planning needed). |
| PEEK | — | High-performance: chemical/heat resistance; medical implants, aerospace; expensive. |
| ABS | — | Impact resistant, low cost; prototyping and housings. |
| PTFE (Teflon) | — | Near-zero friction, chemical inertness; seals and insulators; hard to hold tolerance. |
Key Properties of Machined Engineering Plastics
- ✓Light weight
- ✓Corrosion-free
- ✓Low friction options
- ✓Electrical insulation
Typical tolerances:±0.1 mm typical; thermal expansion and moisture limit precision
Applications for Engineering Plastics Parts
- Gears and bushings
- Insulators
- Seals and wear strips
- Medical device components (PEEK)
- Enclosures and jigs
Machining Notes for Engineering Plastics
Sharp positive-rake tools, moderate speeds, air blast or coolant; watch heat buildup (melting) and clamping pressure (deformation).
Finishes for Engineering Plastics Parts
- As-machined (typical)
- Vapor polishing (select plastics)
- Dyeing
Keupayaan
- Pemesinan ABS/POM/nilon/PEEK/PTFE mengikut lukisan
- Strategi alat tajam menentang pencairan dan pengepingan
- Pengilatan nyalaan dan buff akrilik
- Penyelarasan penyepuhlindapan untuk pelepasan tegasan
Bahan biasa
ABS, POM-C (Delrin), Nilon 6/6, PEEK, PTFE, HDPE/UHMW, polikarbonat, akrilik (PMMA).
| Bahan / gred | Keadaan lazim | Kebolehmahinan | Sesuai untuk |
|---|---|---|---|
| Aluminium 6061 | T6 (larutan haba dan ditua) | Mudah: mudah dipotong, kawalan serpihan baik | Penyangkut, rumah, kelengkapan, prototaip hingga pengeluaran |
| Aluminium 7075 | T6 / T651 | Lebih sukar: haus alat lebih cepat, perlu persediaan tegar | Bahagian berkekuatan tinggi kritikal-berat; tidak untuk kimpalan |
| Keluli tahan karat 304 / 304L | Dilunakan | Mengeras-kerja: kelajuan lebih rendah, suapan positif | Rintangan kakisan am, peralatan makanan dan proses |
| Keluli tahan karat 316 / 316L | Dilunakan | Lebih liat daripada 304: haus alat lebih cepat | Pendedahan klorida, marin, perubatan dan farmaseutikal |
| Keluli karbon 1018 / 1045 | Sebagai-gulung / dinormalisasi | Mudah hingga sederhana; perlu perlindungan daripada karat | Acuan, plat, fabrikasi kimpalan, badan perkakas |
| Loyang C360 | H02 separa keras | Cemerlang: kelajuan tinggi, kemasan bersih | Kelengkapan, bushing, penyambung, bahagian hiasan |
| Kuprum C110 | Dilunakan / H02 | Lekat: alat tajam dan sudut rake tinggi | Kekonduksian, basbar, pengurusan haba |
| Titanium Grade 5 (Ti-6Al-4V) | Dilunakan kilang | Sukar: kelajuan rendah, kawalan haba, haus alat | Aeroangkasa, perubatan dan bahagian ringan berkekuatan tinggi |
| Plastik kejuruteraan (POM, PEEK, PA) | Diekstrusi / dilunakan | Mudah hingga lekat: rahang lembut, perkakas tajam | Penebat, geseran rendah, bahagian kimia dan haus |
Kemasan
Sebagai-mesin, dibuang bur, akrilik dipoles nyalaan/buff, disepuhlindap atas permintaan.
| Kemasan | Apa yang ia lakukan | Nyatakan apabila |
|---|---|---|
| Sebagai-mesin | Tanda alat kekal kelihatan; Ra lazimnya 1.6-3.2 µm | Bahagian hanya perlu berfungsi |
| Blast manik | Permukaan matte seragam, menyembunyikan tanda alat | Bahagian kosmetik sebelum anodisasi |
| Anodisasi Jenis II | Membina lapisan oksida; pilihan warna | Rupa aluminium plus rintangan kakisan dan haus sederhana |
| Anodisasi keras Jenis III | Lapisan oksida lebih tebal dan keras | Permukaan aluminium gelongsor atau terhakis |
| Penukaran kromat | Filem pelindung nipis yang kekal konduktif | Ikatan elektrik atau pembumian pada aluminium |
| Nikel tanpa elektro | Lapisan seragam, keras dan tahan kakisan | Haus plus kakisan, termasuk di dalam lubang |
| Penyaduran zink | Perlindungan kakisan korban yang ekonomi | Bahagian keluli dalam servis dalam bangunan atau terlindung |
| Salutan serbuk | Lapisan tebal, tahan lama dan hiasan | Rupa adalah keperluannya |
| Pasivasi | Membuang besi bebas dan memulihkan filem oksida | Bahagian keluli tahan karat selepas pemesinan |
| Legaan tegasan / rawatan haba | Melegakan tegasan baki sebelum atau selepas pemotongan | Dinding nipis dan toleran ketat yang mesti bertahan pemesinan |
Toleran
Am ISO 2768-m; ±0.05 mm lazim, ±0.02 mm pada ciri kritikal.
| Keterangan lukisan | Apa yang diperlukan | Kesan pada kos dan tempoh |
|---|---|---|
| Am: ±0.25 mm / ±0.010 in | Perkakas standard, semakan dimensi | Garis dasar: tiada tambahan |
| Standard: ±0.13 mm / ±0.005 in | Mesin dalam keadaan baik, semakan artikel pertama | Tambahan kecil; lalai lazim sebut harga |
| Ketat: ±0.025 mm / ±0.001 in | Perkakas digilap atau berlian, kawalan suhu, CMM | Perubahan langkah: pemotongan lebih perlahan plus pemeriksaan penuh |
| Berketepatan tinggi: ±0.013 mm / ±0.0005 in | Laluan kemasan, tolok, persekitaran terkawal | Pemesinan mendominasi harga; sering operasi berasingan |
| Kedudukan / kecondongan (GD&T) | Kawalan datum, satu persediaan jika ciri berkaitan | Bergantung pada bilangan persediaan yang diliputi datum |
| Kemasan permukaan Ra 0.8 µm atau lebih halus | Langkah sanding lebih halus, pengilatan atau laluan kemasan | Menambah satu langkah proses, bukan sekadar masa pemesinan |
Related Processes
5-axis CNC machining
used for
CNC Milling
used for
Recycling
used for
Common Applications
- Turning
- cost-sensitive prototypes
- consumer goods
Pilihan Proses
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Soalan yang sering diajukan
PEEK atau Delrin untuk aplikasi saya?
Delrin (POM-C) sesuai untuk bahagian mekanikal berketepatan tinggi pada kos sederhana; PEEK sesuai untuk suhu tinggi, pensterilan dan pendedahan kimia pada harga premium. Kami mengesyorkan berdasarkan persekitaran operasi.
Mengapa toleran plastik lebih longgar daripada logam?
Plastik mengembang dan mengendur dengan suhu dan tegasan kira-kira sepuluh kali lebih daripada logam. ±0.05 mm adalah lazim; kami mengekalkan ±0.02 mm pada ciri kritikal dengan bahan stabil dan proses terkawal.
Bolehkah anda memesin bahagian akrilik lutsinar?
Ya. Kami memesin akrilik dengan alat tajam dan mengilatnya sehingga lutsinar di mana geometri membenarkan — hantar lukisan dan nyatakan muka mana yang mesti kekal jernih secara optik.
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- hubs.comIndustry peer technical page
- xometry.comIndustry peer technical page
- uneedpm.comUnclassified source
- us.arrk.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Perkhidmatan berkaitan
Capability commitments on this page are owner-confirmed (2026-09-21).