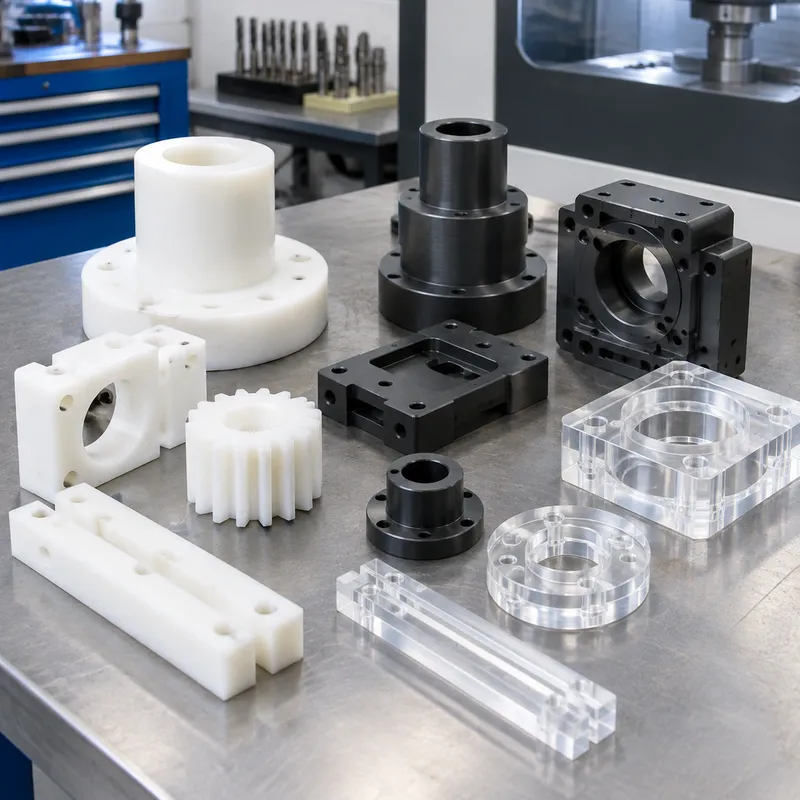
당사가 가공하는 플라스틱 부품은 시제품, 절연체, 기어, 부싱, 내마모 부품, 의료용 등급 PEEK 부품, 광학용 아크릴 렌즈를 아울립니다. 일반 용도에는 ABS와 POM(델린), 내마모에는 나일론 6/6, 내열 및 멸균에는 PEEK, 내화학 및 저마찰 용도에는 PTFE를 사용합니다.
플라스틱은 금속과 다르게 가공됩니다. 열팽창이 약 10배 크고 열이 빠르게 축적되므로, 당사는 날카롭게 연마된 공구, 보수적인 절삭 속도, 다운(클라임) 밀링으로 가장자리의 용융이나 파손을 방지합니다. 공차는 재질의 특성을 반영해 현실적으로 잡습니다.
Material Grades & Properties
Engineering Plastics Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| POM (Delrin/Acetal) | — | Low friction, high stiffness, dimensional stability; gears, bushings, precision parts. |
| Nylon (PA6/PA66) | — | Tough and wear-resistant; absorbs moisture (dimension planning needed). |
| PEEK | — | High-performance: chemical/heat resistance; medical implants, aerospace; expensive. |
| ABS | — | Impact resistant, low cost; prototyping and housings. |
| PTFE (Teflon) | — | Near-zero friction, chemical inertness; seals and insulators; hard to hold tolerance. |
Key Properties of Machined Engineering Plastics
- ✓Light weight
- ✓Corrosion-free
- ✓Low friction options
- ✓Electrical insulation
Typical tolerances:±0.1 mm typical; thermal expansion and moisture limit precision
Applications for Engineering Plastics Parts
- Gears and bushings
- Insulators
- Seals and wear strips
- Medical device components (PEEK)
- Enclosures and jigs
Machining Notes for Engineering Plastics
Sharp positive-rake tools, moderate speeds, air blast or coolant; watch heat buildup (melting) and clamping pressure (deformation).
Finishes for Engineering Plastics Parts
- As-machined (typical)
- Vapor polishing (select plastics)
- Dyeing
생산 역량
- ABS/POM/나일론/PEEK/PTFE 도면 기준 가공
- 용융 및 파손 방지를 위한 샤프 공구 전략
- 아크릴 화염 및 버프 연마
- 응력 제거를 위한 어닐링 협조 대응
대표 소재
ABS, POM-C(델린), 나일론 6/6, PEEK, PTFE, HDPE/UHMW, 폴리카보네이트, 아크릴(PMMA).
| 재질 / 등급 | 일반적인 상태 | 절삭 가공성 | 적합한 용도 |
|---|---|---|---|
| Aluminium 6061 | T6(용체화 처리 및 시효 경화) | 용이함: 절삭성이 좋고 칩 배출이 안정적 | 브래킷, 하우징, 지그, 시제품부터 양산까지 |
| Aluminium 7075 | T6 / T651 | 다소 어려움: 공구 마모가 크고 강성 높은 셋업이 필요 | 고강도·경량이 중요한 부품. 용접에는 부적합 |
| Stainless 304 / 304L | 어닐링 | 가공 경화됨: 저속 절삭, 플러스 레이크 방식 | 일반 내식성. 식품·공정 설비 |
| Stainless 316 / 316L | 어닐링 | 304보다 점성이 높음: 공구 마모 증가 | 염화물 환경, 해양, 의료·제약 용도 |
| Carbon steel 1018 / 1045 | 압연 / 노멀라이징 | 보통: 녹 방지 처리 필요 | 축, 판재, 용접 구조물, 공구 바디 |
| Brass C360 | H02 반경질 | 매우 용이함: 고속 절삭에서 깔끔한 표면 마감 | 피팅, 부싱, 커넥터, 장식 부품 |
| Copper C110 | 어닐링 / H02 | 점착성: 날카로운 공구와 큰 경사각 필요 | 전도성, 부스바, 열 관리 |
| Titanium Grade 5 (Ti-6Al-4V) | 밀 어닐링 | 어려움: 저속 절삭, 열 관리, 공구 마모 | 항공우주, 의료, 경량 고강도 부품 |
| 엔지니어링 플라스틱(POM, PEEK, PA) | 압출 / 어닐링 | 용이함부터 점착성까지: 소프트 조와 날카로운 공구 | 절연, 저마찰, 내화학·내마모 부품 |
표면처리
가공 원상태, 버 제거, 아크릴 화염/버프 연마, 어닐링(요청 시).
| 표면 처리 | 효과 | 지정하면 좋은 경우 |
|---|---|---|
| 절삭 마감 그대로 | 공구 자국이 남음. Ra 통상 1.6-3.2 µm | 기능만 충족하면 되는 부품 |
| 비드 블라스트 | 균일한 무광 표면. 공구 자국을 흐려 줌 | 양극산화 전의 외관 부품 |
| 양극산화 Type II | 산화 피막을 형성. 색상 선택 가능 | 알루미늄 외관과 중간 수준의 내식·내마모가 필요할 때 |
| 경질 양극산화 Type III | 더 두껍고 단단한 산화 피막 | 미끄러지거나 마모되는 알루미늄 표면 |
| 크로메이트 처리 | 도전성을 유지하는 얇은 보호 피막 | 알루미늄의 전기적 접속 또는 접지 |
| 무전해 니켈 도금 | 균일하고 단단하며 내식성 있는 피막 | 마모와 부식 모두에 대응. 보어 내면 포함 |
| 아연 도금 | 경제적인 희생 양극 방식의 방식 처리 | 실내 또는 보호된 환경의 강재 부품 |
| 분체 도장 | 두껍고 내구성 있는 장식 피막 | 외관이 요구 사항일 때 |
| 부동태 처리 | 유리 철을 제거하고 산화 피막을 회복 | 가공 후 스테인리스 부품 |
| 잔류 응력 제거 / 열처리 | 가공 전후의 잔류 응력을 제거 | 가공을 견뎌야 하는 박육·조공차 부품 |
공차
ISO 2768-m 일반; ±0.05 mm 일반적, 핵심 형상 기준 ±0.02 mm.
| 도면 공차 표기 | 필요한 조건 | 비용과 납기에 미치는 영향 |
|---|---|---|
| 일반: ±0.25 mm / ±0.010 in | 표준 공구, 치수 검사 | 기준선: 추가 비용 없음 |
| 표준: ±0.13 mm / ±0.005 in | 양호한 상태의 공작기계, 초기 품질 검사 | 소폭 추가. 일반적인 견적 기준 |
| 조밀: ±0.025 mm / ±0.001 in | 연삭 또는 다이아몬드 공구, 온도 관리, CMM | 단계적 상승: 절삭 속도 저하 및 전수 검사 |
| 정밀: ±0.013 mm / ±0.0005 in | 마감 패스, 게이지, 환경 관리 | 가공 비용이 가격을 지배. 별도 공정인 경우가 많음 |
| 위치도 / 각도 공차 (GD&T) | 데이텀 관리, 관련 형상은 한 번의 셋업에서 가공 | 데이텀이 걸치는 셋업 수에 따라 달라짐 |
| 표면 조도 Ra 0.8 µm 이하 | 더 미세한 패스, 연마 또는 마감 패스 | 가공 시간만이 아니라 공정이 하나 추가됨 |
Related Processes
5-axis CNC machining
used for
CNC Milling
used for
Recycling
used for
Common Applications
- Turning
- cost-sensitive prototypes
- consumer goods
공정 옵션
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
자주 묻는 질문
우리 용도에는 PEEK와 델린 중 무엇이 적합한가요?
델린(POM-C)은 적정 비용의 정밀 기계 부품에 적합하고, PEEK는 고온, 멸균, 내화학이 필요한 용도에 프리미엄으로 적합합니다. 사용 환경을 기준으로 권장해 드립니다.
플라스틱 공차가 금속보다 넓은 이유는 무엇인가요?
플라스틱은 온도와 응력에 따라 금속의 약 10배로 팽창하고 이완됩니다. ±0.05 mm가 일반적이며, 안정된 재질과 제어된 공정으로 핵심 형상은 ±0.02 mm까지 유지합니다.
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- hubs.comIndustry peer technical page
- xometry.comIndustry peer technical page
- uneedpm.comUnclassified source
- us.arrk.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Capability commitments on this page are owner-confirmed (2026-09-21).