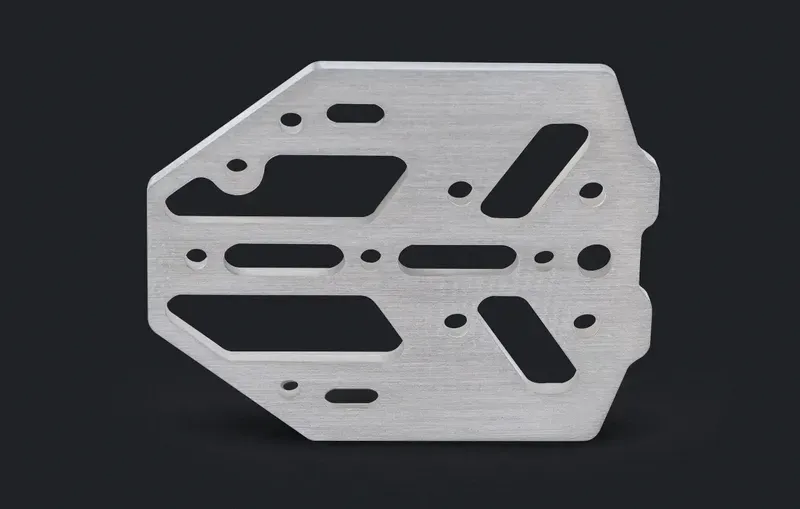
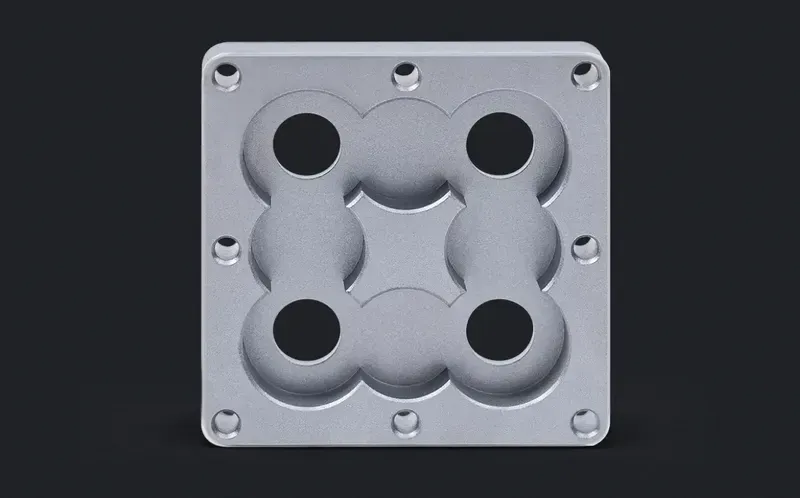
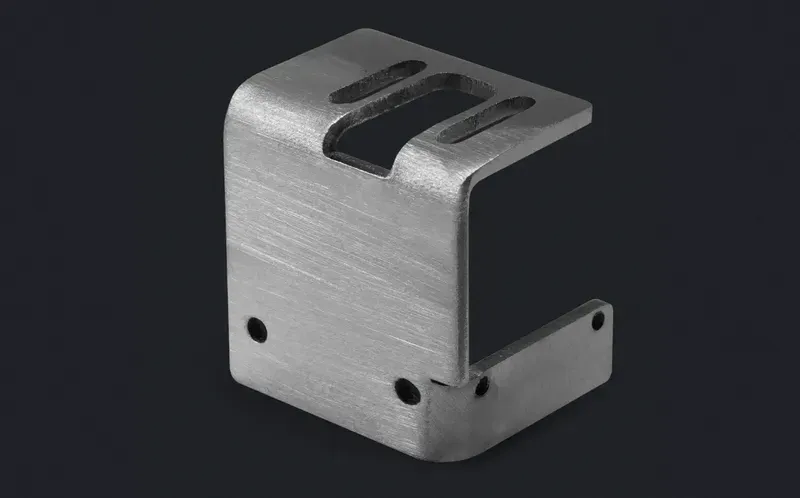
हमारे द्वारा मशीन किए जाने वाले स्टेनलेस स्टील पार्ट्स फ़ूड-कॉन्टैक्ट फ़िटिंग, मरीन हार्डवेयर, मेडिकल-शैली कंपोनेंट और औद्योगिक उपकरण कवर करते हैं: फ़्री-मशीनिंग फ़िटिंग के लिए 303, सामान्य संक्षारण प्रतिरोध के लिए 304, क्लोराइड और मरीन वातावरण के लिए 316L, जहाँ शक्ति मायने रखे वहाँ 17-4PH।
सही ग्रेड चयन, टूल पाथ और पैसिवेशन ही स्टेनलेस पार्ट्स को फ़ील्ड में प्रदर्शन देते हैं — DFM समीक्षा के दौरान हम संक्षारण-संबंधी कॉलआउट चिह्नित करते हैं।
मुख्य विनिर्देश
| Specification | Value |
|---|---|
| lead time | 7 days |
| tolerance | ±0.002 in |
| lead time | 80 days |
| lead time | 120 days |
| surface finish | Ra0.6 |
Material Grades & Properties
Stainless Steel Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| 304 | ASTM A240 | General purpose austenitic; excellent corrosion resistance; work-hardens. |
| 316/316L | ASTM A240 | Added molybdenum for chloride resistance; marine and medical use. |
| 17-4 PH | ASTM A564 | Precipitation hardening; high strength after heat treatment; aerospace/medical. |
| 303 | ASTM A582 | Sulfur-added free-machining grade; best machinability of austenitic; lower corrosion resistance. |
Key Properties of Machined Stainless Steel
- ✓Corrosion resistance
- ✓High strength
- ✓Heat resistance
- ✓Hygienic (food/medical compatible grades)
Typical tolerances:±0.05 mm standard; ±0.01 mm achievable with finishing
Applications for Stainless Steel Parts
- Medical instruments and implants
- Food processing equipment
- Marine hardware
- Valves and fittings
- Aerospace components
Machining Notes for Stainless Steel
Work-hardens quickly: maintain consistent feed, sharp tooling, adequate coolant. 303 machines easiest; 316 slowest of the common grades.
Finishes for Stainless Steel Parts
- Passivation
- Electropolishing
- Bead blasting
- Vibratory finishing
क्षमताएँ
- 303/304/316L/17-4PH ड्रॉइंग अनुसार मशीनिंग
- ग्राहक विनिर्देश अनुसार पैसिवेशन
- अनुरोध पर इलेक्ट्रोपॉलिशिंग
- एक सेटअप में थ्रेड और फ़िटिंग ज्यामिति
सामान्य सामग्रियाँ
स्टेनलेस 303, 304, 316/316L, 17-4PH, 410, 416, अनुरोध पर डुप्लेक्स।
| सामग्री / ग्रेड | सामान्य अवस्था | मशीनेबिलिटी | कहाँ उपयुक्त |
|---|---|---|---|
| Aluminium 6061 | T6 (सॉल्यूशन ट्रीटेड और एज्ड) | आसान: फ़्री-कटिंग, अच्छा चिप नियंत्रण | ब्रैकेट, हाउसिंग, फ़िक्स्चर, प्रोटोटाइप से उत्पादन तक |
| Aluminium 7075 | T6 / T651 | कठिन: अधिक टूल घिसाव, दृढ़ सेटअप आवश्यक | उच्च-शक्ति, वज़न-महत्वपूर्ण पार्ट्स; वेल्डिंग के लिए नहीं |
| Stainless 304 / 304L | एनील्ड | वर्क-हार्डन करता है: धीमी गति, पॉज़िटिव फ़ीड | सामान्य संक्षारण प्रतिरोध, फ़ूड और प्रोसेस उपकरण |
| Stainless 316 / 316L | एनील्ड | 304 से अधिक टफ़: अधिक टूल घिसाव | क्लोराइड, मरीन, मेडिकल और फ़ार्मा परिस्थितियाँ |
| कार्बन स्टील 1018 / 1045 | अस-रोल्ड / नॉर्मलाइज़्ड | आसान से मध्यम; जंग से सुरक्षा आवश्यक | शाफ़्ट, प्लेट, वेल्डमेंट, टूलिंग बॉडी |
| पीतल C360 | H02 हाफ़ हार्ड | उत्कृष्ट: उच्च गति, साफ़ फ़िनिश | फ़िटिंग, बुशिंग, कनेक्टर, डेकोरेटिव पार्ट्स |
| तांबा C110 | एनील्ड / H02 | गमी: तेज़ टूल और बड़े रेक कोण आवश्यक | कंडक्टिविटी, बसबार, थर्मल मैनेजमेंट |
| टाइटेनियम Grade 5 (Ti-6Al-4V) | मिल एनील्ड | कठिन: कम गति, ताप नियंत्रण, टूल घिसाव | एयरोस्पेस, मेडिकल और हल्के उच्च-शक्ति पार्ट्स |
| इंजीनियरिंग प्लास्टिक (POM, PEEK, PA) | एक्सट्रूडेड / एनील्ड | आसान से गमी: सॉफ़्ट जॉ, तेज़ टूलिंग | इंसुलेशन, कम घर्षण, केमिकल और वियर पार्ट्स |
फ़िनिश
पैसिवेशन, इलेक्ट्रोपॉलिशिंग, बीड ब्लास्टिंग, पॉलिशिंग, ब्लैक ऑक्साइड।
| फ़िनिश | यह क्या करती है | कब निर्दिष्ट करें |
|---|---|---|
| अस मशीन्ड | टूल निशान दिखते हैं; Ra सामान्यतः 1.6–3.2 µm | पार्ट को केवल काम करना है |
| बीड ब्लास्ट | एकरूप मैट सतह, टूल निशान छिपाती है | एनोडाइज़िंग से पहले कॉस्मेटिक पार्ट्स |
| एनोडाइज़िंग टाइप II | ऑक्साइड परत बनाती है; रंग विकल्प | एल्युमीनियम रूप प्लस हल्का संक्षारण और वियर प्रतिरोध |
| हार्ड एनोडाइज़िंग टाइप III | मोटी, कठोर ऑक्साइड परत | स्लाइडिंग या घिसने वाली एल्युमीनियम सतहें |
| क्रोमेट कन्वर्ज़न | पतली सुरक्षात्मक फ़िल्म जो कंडक्टिव रहती है | एल्युमीनियम पर इलेक्ट्रिकल बॉन्डिंग या ग्राउंडिंग |
| इलेक्ट्रोलेस निकल | एकरूप, कठोर, संक्षारण-रोधी परत | वियर प्लस संक्षारण, बोर के अंदर भी |
| ज़िंक प्लेटिंग | किफ़ायती त्यागी संक्षारण सुरक्षा | इनडोर या आश्रित सेवा में स्टील पार्ट्स |
| पाउडर कोट | मोटी, टिकाऊ, डेकोरेटिव परत | जब रूप ही आवश्यकता हो |
| पैसिवेशन | फ़्री आयरन हटाकर ऑक्साइड फ़िल्म बहाल करती है | मशीनिंग के बाद स्टेनलेस पार्ट्स |
| स्ट्रेस रिलीफ़ / हीट ट्रीटमेंट | कटिंग से पहले या बाद अवशिष्ट तनाव घटाती है | पतली दीवारें और कड़े टॉलरेंस जो मशीनिंग से बचने चाहिए |
टॉलरेंस
ISO 2768-m मानक; महत्वपूर्ण फ़ीचर पर ±0.01 mm।
| कॉलआउट | इसे क्या चाहिए | लागत और लीड टाइम पर प्रभाव |
|---|---|---|
| सामान्य: ±0.25 mm / ±0.010 in | मानक टूलिंग, डायमेंशनल जाँच | आधारभूत: कोई अतिरिक्त शुल्क नहीं |
| मानक: ±0.13 mm / ±0.005 in | अच्छी स्थिति में मशीन, फ़र्स्ट-आर्टिकल जाँच | थोड़ा अतिरिक्त शुल्क; सामान्य कोटिंग डिफ़ॉल्ट |
| कड़ा: ±0.025 mm / ±0.001 in | ग्राइंडेड या डायमंड टूलिंग, तापमान नियंत्रण, CMM | स्तर-परिवर्तन: धीमी कटिंग प्लस पूर्ण निरीक्षण |
| प्रिसिजन: ±0.013 mm / ±0.0005 in | फ़िनिश पास, गेजिंग, नियंत्रित वातावरण | मशीनिंग कीमत तय करती है; अक्सर अलग ऑपरेशन |
| पोज़िशन / एंगुलैरिटी (GD&T) | डेटम नियंत्रण, संबंधित फ़ीचर के लिए एक सेटअप | इस पर निर्भर करता है कि डेटम कितने सेटअप फैलाता है |
| सरफ़ेस फ़िनिश Ra 0.8 µm या महीन | महीन स्टेपओवर, पॉलिशिंग या फ़िनिशिंग पास | केवल मशीनिंग समय नहीं, एक प्रक्रिया चरण जुड़ता है |
Materials We Machine
- Brass
- Copper
- Stainless Steel 201
- Titanium
- iron
- molybdenum
- nickel-pig-iron
- raw materials
- steel
Common Applications
- Airplane Parts
- Chemical Housings
- Cover
- Decorative/Architectural
- Equipment Panels
- Food parts
- Food-Contact
- Freshwater Environment
- Marine Parts
- Marine hardware
- Medical Machines
- Micro Mechanical Parts
- Oxidizing Environment
- Stainless Steel CNC Machining
- Water Pipes
- Weak Acids
- architectural design
- chloride-rich environments
- city buildings
- corrosive process environments
- critical fasteners
- dive watch
- folding hinges
- food machines
प्रक्रिया विकल्प
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
सामान्य प्रश्न
मरीन वातावरण के लिए कौन-सा स्टेनलेस ग्रेड?
क्लोराइड एक्सपोज़र के लिए 316L डिफ़ॉल्ट है। उच्च-शक्ति मरीन हार्डवेयर के लिए H900 कंडीशन में 17-4PH सामान्य है; अपने वातावरण डेटा से पुष्टि करें।
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- seathertechnology.comUnclassified source
- fictiv.comIndustry peer technical page
- actionstainless.comUnclassified source
- yshsteel.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Related Knowledge
Capability commitments on this page are owner-confirmed (2026-09-21).