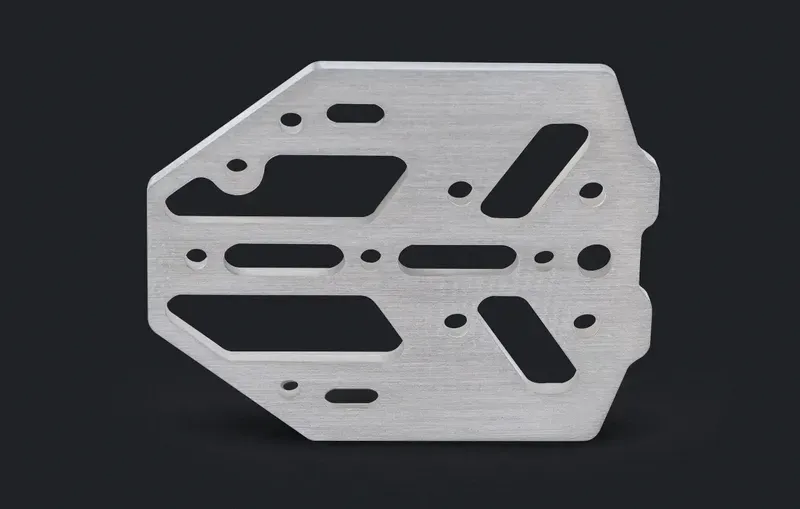
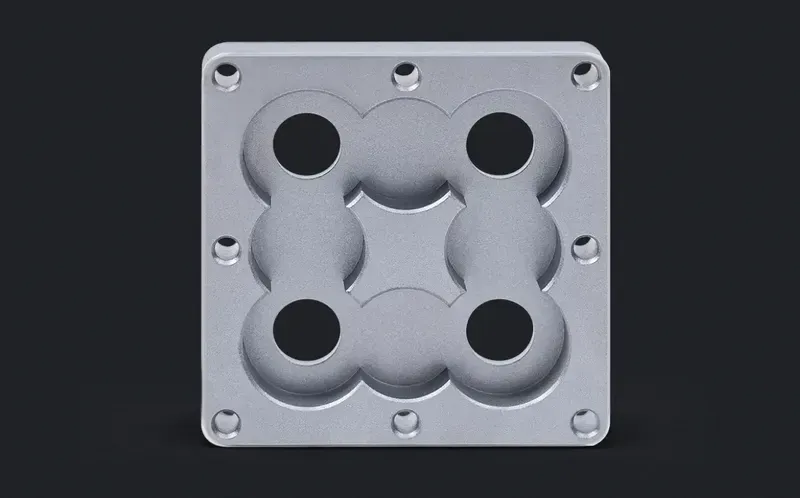
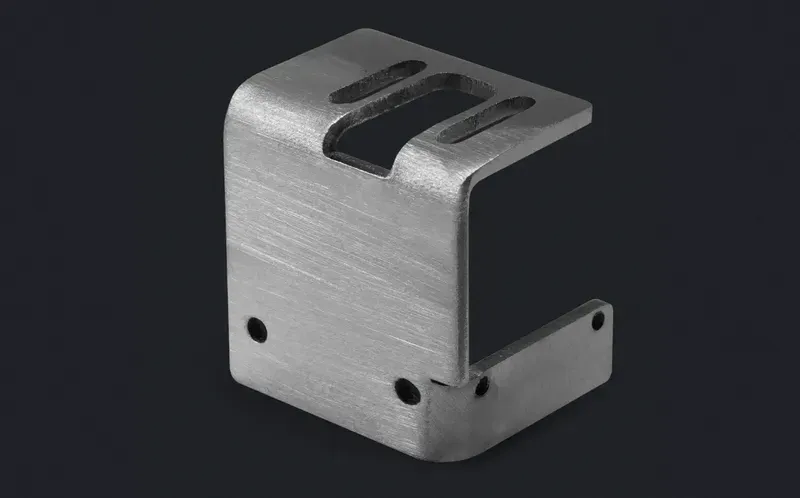
Деталі з нержавіючої сталі, які ми обробляємо, охоплюють фітинги для контакту з харчовими продуктами, морську арматуру, компоненти медичного типу та промислове обладнання: 303 для легкооброблюваних фітингів, 304 для загальної корозійної стійкості, 316L для хлоридних і морських середовищ, 17-4PH там, де важлива міцність.
Правильний вибір марки, траєкторій інструменту та пасивація — саме те, що робить деталі з нержавійки надійними в експлуатації. Ми позначаємо критичні для корозії позначки під час DFM-огляду.
Ключові характеристики
| Specification | Value |
|---|---|
| lead time | 7 days |
| tolerance | ±0.002 in |
| lead time | 80 days |
| lead time | 120 days |
| surface finish | Ra0.6 |
Material Grades & Properties
Stainless Steel Grades We Machine
| Grade | Standard | Characteristics |
|---|---|---|
| 304 | ASTM A240 | General purpose austenitic; excellent corrosion resistance; work-hardens. |
| 316/316L | ASTM A240 | Added molybdenum for chloride resistance; marine and medical use. |
| 17-4 PH | ASTM A564 | Precipitation hardening; high strength after heat treatment; aerospace/medical. |
| 303 | ASTM A582 | Sulfur-added free-machining grade; best machinability of austenitic; lower corrosion resistance. |
Key Properties of Machined Stainless Steel
- ✓Corrosion resistance
- ✓High strength
- ✓Heat resistance
- ✓Hygienic (food/medical compatible grades)
Typical tolerances:±0.05 mm standard; ±0.01 mm achievable with finishing
Applications for Stainless Steel Parts
- Medical instruments and implants
- Food processing equipment
- Marine hardware
- Valves and fittings
- Aerospace components
Machining Notes for Stainless Steel
Work-hardens quickly: maintain consistent feed, sharp tooling, adequate coolant. 303 machines easiest; 316 slowest of the common grades.
Finishes for Stainless Steel Parts
- Passivation
- Electropolishing
- Bead blasting
- Vibratory finishing
Можливості
- Обробка 303/304/316L/17-4PH за креслеником
- Пасивація за специфікацією замовника
- Електрополірування на запит
- Різьба та геометрія фітингів за одного встановлення
Типові матеріали
Нержавіюча сталь 303, 304, 316/316L, 17-4PH, 410, 416, дуплекс на запит.
| Матеріал / марка | Типовий стан постачання | Оброблюваність | Де застосовується |
|---|---|---|---|
| Aluminium 6061 | T6 (гартування зі старінням) | Легко: вільно ріжеться, хороший контроль стружки | Кронштейни, корпуси, оснащення, прототипи з переходом у серію |
| Aluminium 7075 | T6 / T651 | Важче: більший знос інструменту, потрібні жорсткі налагодження | Високоміцні деталі з критичною масою; не для зварювання |
| Stainless 304 / 304L | Відпалений | Наклепується: менші швидкості, позитивна подача | Загальна корозійна стійкість, харчове та технологічне обладнання |
| Stainless 316 / 316L | Відпалений | Міцніший за 304: більший знос інструменту | Хлориди, морське середовище, медичне та фармацевтичне обладнання |
| Carbon steel 1018 / 1045 | Гарячекатаний / нормалізований | Від легкого до середнього; потрібен захист від корозії | Вали, плити, зварні конструкції, корпуси оснащення |
| Brass C360 | H02 напівтвердий | Відмінно: високі швидкості, чиста поверхня | Фітинги, втулки, з'єднувачі, декоративні деталі |
| Copper C110 | Відпалений / H02 | В'язкий: гострі інструменти та великі передні кути | Електропровідність, струмопроводи, термоменеджмент |
| Titanium Grade 5 (Ti-6Al-4V) | Міцність у стані поставки (mill annealed) | Важко: малі швидкості, контроль нагріву, знос інструменту | Аерокосмічна галузь, медицина, легкі високоміцні деталі |
| Конструкційні пластики (POM, PEEK, PA) | Екструдований / відпалений | Від легкого до в'язкого: м'які губки, гострий інструмент | Ізоляція, низьке тертя, хімічно- та зносостійкі деталі |
Покриття
Пасивація, електрополірування, дробеструйна обробка, полірування, воронення.
| Покриття | Що воно дає | Коли вказувати |
|---|---|---|
| Після обробки | Сліди інструменту залишаються видимими; Ra зазвичай 1.6-3.2 µm | Деталь має просто виконувати свою функцію |
| Дробеструйна обробка | Рівномірна матова поверхня, приховує сліди інструменту | Декоративні деталі перед анодуванням |
| Анодування Type II | Створює оксидний шар; варіанти кольору | Вигляд алюмінію плюс помірна корозійна та зносостійкість |
| Тверде анодування Type III | Більш товстий і твердий оксидний шар | Зковзуючі або зношувані алюмінієві поверхні |
| Хроматне конверсійне покриття | Тонка захисна плівка, що зберігає провідність | Електричне з'єднання або заземлення на алюмінії |
| Хімічне нікелювання | Рівномірний, твердий, корозійностійкий шар | Знос плюс корозія, зокрема всередині отворів |
| Цинкування | Економічний жертовний захист від корозії | Сталеві деталі в приміщеннях або під навісом |
| Порошкове фарбування | Товстий, довговічний, декоративний шар | Коли вимогою є саме зовнішній вигляд |
| Пасивація | Видаляє вільне залізо та відновлює оксидну плівку | Деталі з нержавіючої сталі після обробки |
| Відпуск для зняття напружень / термообробка | Знімає залишкові напруження до або після різання | Тонкі стінки та жорсткі допуски, що мають пережити обробку |
Допуски
Стандарт ISO 2768-m; ±0.01 mm на критичних елементах.
| Допуск на кресленику | Що він вимагає | Вплив на вартість і термін |
|---|---|---|
| Загальний: ±0.25 mm / ±0.010 in | Стандартний інструмент, розмірна перевірка | Базовий рівень: без надбавки |
| Стандартний: ±0.13 mm / ±0.005 in | Верстат у доброму стані, перевірка першої деталі | Невелика надбавка; звичайна база для розрахунку |
| Жорсткий: ±0.025 mm / ±0.001 in | Шліфований або алмазний інструмент, контроль температури, КВМ | Стрибок: повільніші проходи плюс повний контроль |
| Точний: ±0.013 mm / ±0.0005 in | Чистові проходи, калібри, контрольоване середовище | Обробка визначає ціну; часто окрема операція |
| Позиція / кутовість (GD&T) | Контроль баз, одне встановлення для пов'язаних елементів | Залежить від того, скільком встановленням охоплюється база |
| Шорсткість поверхні Ra 0.8 µm або дрібніше | Дрібніші кроки, полірування або чистовий прохід | Додає етап процесу, а не лише час обробки |
Materials We Machine
- Brass
- Copper
- Stainless Steel 201
- Titanium
- iron
- molybdenum
- nickel-pig-iron
- raw materials
- steel
Common Applications
- Airplane Parts
- Chemical Housings
- Cover
- Decorative/Architectural
- Equipment Panels
- Food parts
- Food-Contact
- Freshwater Environment
- Marine Parts
- Marine hardware
- Medical Machines
- Micro Mechanical Parts
- Oxidizing Environment
- Stainless Steel CNC Machining
- Water Pipes
- Weak Acids
- architectural design
- chloride-rich environments
- city buildings
- corrosive process environments
- critical fasteners
- dive watch
- folding hinges
- food machines
Варіанти обробки
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Часті запитання
Яка марка нержавіючої сталі для морського середовища?
316L — стандартний вибір для впливу хлоридів. Для високоміцної морської арматури поширений 17-4PH у стані H900; підтвердьте даними про ваше середовище.
What is the minimum order quantity (MOQ)?
Prototypes from 1 pc. Low-volume production typical 50-500 pcs. No forced MOQ on custom parts; unit price drops with volume.
What is the typical lead time?
Industry benchmark: instant-quote platforms deliver prototypes in 1-3 business days. Our own production: prototypes 5-10 working days, including in-house QC and shipping. Production: 2-4 weeks depending on quantity/finishing. Express options exist; finishing adds days.
How do I get a quote and what information do you need?
3D files (STEP/IGS) + 2D drawing with tolerances. Material, quantity, finish, destination country. Quote turnaround: 24-48h typical.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 4
- seathertechnology.comUnclassified source
- fictiv.comIndustry peer technical page
- actionstainless.comUnclassified source
- yshsteel.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Related Knowledge
Capability commitments on this page are owner-confirmed (2026-09-21).