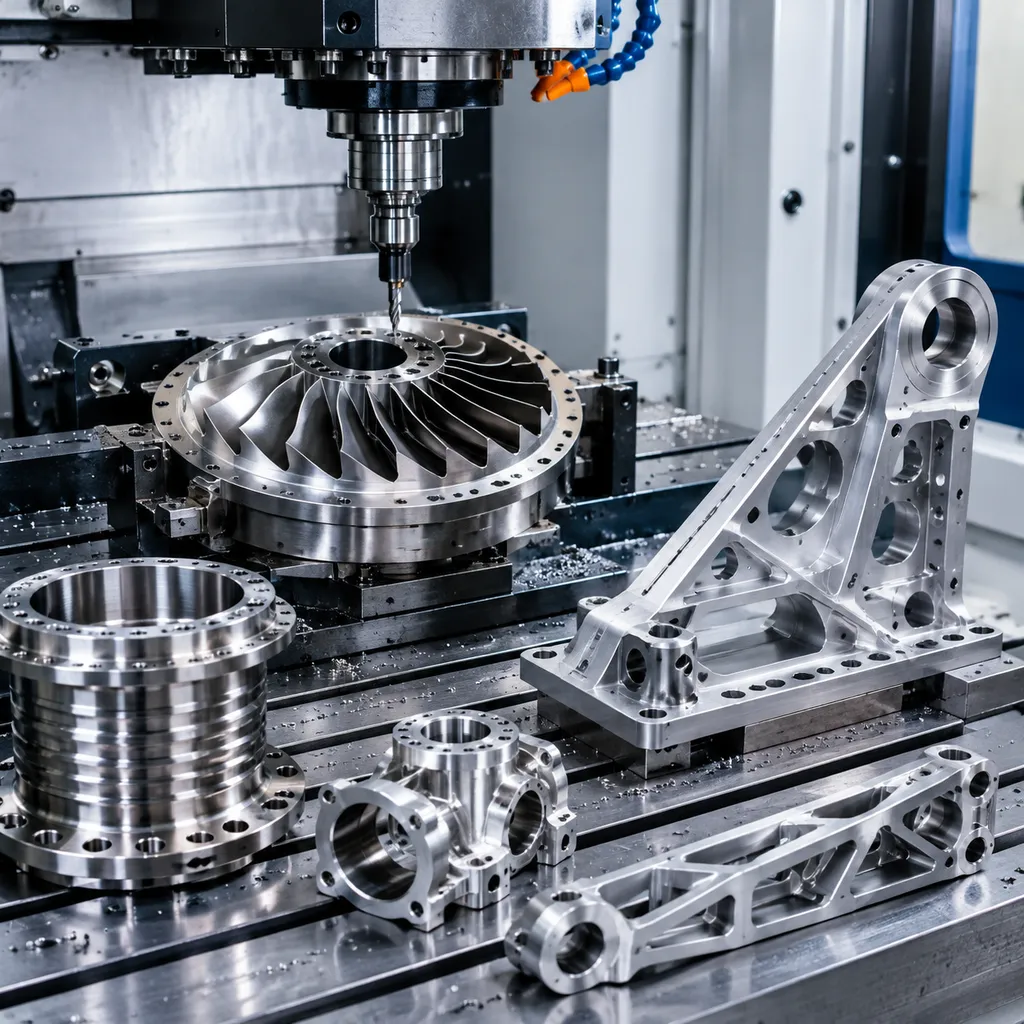
Aerospace machining is the precision CNC manufacture of components for aircraft, spacecraft, satellites, and unmanned systems — parts such as structural fittings, engine mounts, housings, and fasteners where tolerances, material integrity, and traceability are critical. Typical work spans 3-axis milling, multi-axis machining, and turning in aluminum, titanium, and stainless steel. Unlike general industrial machining, aerospace parts must meet strict engineering drawings, material certifications, and inspection requirements, and often involve complex geometries that demand 5-axis capability and disciplined process control from first article through production.
For aerospace buyers, the value lies in de-risking the supply chain. We machine to your drawing on equipment and inspection processes matched to aerospace requirements, so you spend less time auditing suppliers and more time managing programs. Whether you need a five-piece prototype batch or ongoing production of machined fittings and housings, one team handles the job from quote to delivery — with comparable quotes, consistent documentation and a single point of coordination.
Getting started is straightforward: submit an RFQ with your 3D models (STEP or IGES), 2D drawings with tolerances and key characteristics, and any special requirements such as material certifications, surface finishes, or export control restrictions. Our engineering team reviews your request and typically returns quotations within a few business days. You can order first articles with full inspection reports before committing to production volumes. Throughout the program, our team coordinates documentation and delivery scheduling so nothing is lost between your engineering team and the shop floor.
Capabilities
- 3-, 4-, and 5-axis milling for complex aerospace geometries and structural parts
- CNC turning of bushings, fittings, and rotational components up to production volumes
- Machining of aluminum, titanium, stainless steel, and high-temperature aerospace alloys
- Tight-tolerance work to ±0.005 mm on critical dimensions with CMM verification
- First article inspection with dimensional reports, material certs, and full traceability
- Prototyping through low-volume production with design-for-manufacturability feedback on request
Typical materials
Common materials include aluminum 2024, 6061, 7050, and 7075; titanium Grade 2 and Grade 5 (Ti-6Al-4V); stainless steel 303, 304, 316, 15-5 PH, and 17-4 PH; nickel alloys such as Inconel 625 and 718; plus magnesium and engineering plastics, with mill-traceable material certifications available on request.
| Material / grade | Typical condition | Machinability | Where it fits |
|---|---|---|---|
| Aluminium 6061 | T6 (solution treated and aged) | Easy: free-cutting, good chip control | Brackets, housings, fixtures, prototypes into production |
| Aluminium 7075 | T6 / T651 | Harder: more tool wear, needs rigid setups | High-strength, weight-critical parts; not for welding |
| Stainless 304 / 304L | Annealed | Work-hardens: slower speeds, positive feed | General corrosion resistance, food and process equipment |
| Stainless 316 / 316L | Annealed | Tougher than 304: more tool wear | Chloride, marine, medical and pharmaceutical exposure |
| Carbon steel 1018 / 1045 | As-rolled / normalised | Easy to moderate; needs protection against rust | Shafts, plates, weldments, tooling bodies |
| Brass C360 | H02 half hard | Excellent: high speeds, clean finish | Fittings, bushings, connectors, decorative parts |
| Copper C110 | Annealed / H02 | Gummy: sharp tools and high rake angles | Conductivity, busbars, thermal management |
| Titanium Grade 5 (Ti-6Al-4V) | Mill annealed | Difficult: low speeds, heat control, tool wear | Aerospace, medical and lightweight high-strength parts |
| Engineering plastics (POM, PEEK, PA) | Extruded / annealed | Easy to gummy: soft jaws, sharp tooling | Insulation, low friction, chemical and wear parts |
Finishes
Available finishes include Type II and Type III (hard) anodizing, chemical conversion coating, passivation, electroless and electrolytic nickel plating, bead blasting, polishing, and industrial painting, applied to drawing and verified before shipment.
| Finish | What it does | Specify it when |
|---|---|---|
| As machined | Tool marks left visible; Ra typically 1.6-3.2 µm | The part only has to function |
| Bead blast | Uniform matte surface, hides tool marks | Cosmetic parts before anodising |
| Anodising Type II | Builds an oxide layer; colour options | Aluminium appearance plus mild corrosion and wear resistance |
| Hard anodising Type III | Thicker, harder oxide layer | Sliding or wearing aluminium surfaces |
| Chromate conversion | Thin protective film that stays conductive | Electrical bonding or grounding on aluminium |
| Electroless nickel | Uniform, hard, corrosion-resistant layer | Wear plus corrosion, including inside bores |
| Zinc plating | Economical sacrificial corrosion protection | Steel parts in indoor or sheltered service |
| Powder coat | Thick, durable, decorative layer | Appearance is the requirement |
| Passivation | Removes free iron and restores the oxide film | Stainless parts after machining |
| Stress relief / heat treatment | Relieves residual stress before or after cutting | Thin walls and tight tolerances that must survive machining |
Tolerances
Standard tolerances follow ISO 2768 medium, while we routinely hold ±0.05 mm (±0.002 in) and can achieve features down to ±0.005 mm (±0.0002 in) depending on part geometry, material, and inspection method.
| Callout | What it needs | Effect on cost and lead time |
|---|---|---|
| General: ±0.25 mm / ±0.010 in | Standard tooling, dimensional check | Baseline: no adder |
| Standard: ±0.13 mm / ±0.005 in | Machine in good condition, first-article check | Small adder; the usual quoting default |
| Tight: ±0.025 mm / ±0.001 in | Ground or diamond tooling, temperature control, CMM | Step change: slower cuts plus full inspection |
| Precision: ±0.013 mm / ±0.0005 in | Finish passes, gauging, controlled environment | Machining dominates the price; often a separate operation |
| Position / angularity (GD&T) | Datum control, one setup where features are related | Depends on how many setups the datum spans |
| Surface finish Ra 0.8 µm or finer | Finer stepovers, polishing or a finishing pass | Adds a process step, not just machining time |
Key Specifications
| Specification | Value |
|---|---|
| tolerance | +/- 0.002 in |
| tolerance | +/- 0.0005 in |
| tolerance | ±0.01 mm |
Process Options
- CNC machining is a subtractive manufacturing process.
- Finishing Options: Black Oxide, Electropolishing, ENP, Media Blasting, Nickel Plating, Passivation, Powder Coating, Tumble Polishing, Zinc Plating, Vibratory Tumbling
- EPX 82 is processed using Carbon DLS
- MUD is a type of mold that uses a standard injection molding frame.
- Different taper turning methods suit different jobs. Compound slides often handle short tapers, while CNC interpolation and taper attachments improve repeatability on longer parts
- G92 is used by programming one or more G92's right after the G76 threading cycle
- Estimates are provided through an auto-quoted method.
- EDM relies on a voltage and a thin wire
- Advanced machining processes like micro-machining and EDM are used to create small, precise mold cavities and cores
Surface Finish Reference
- The finish of MoldTech MT11010 is a fine matte texture.
- The finish of MoldTech MT11020 is a medium matte texture.
- The finish of MoldTech MT11030 is a coarse matte texture.
- SPI A-1 has a surface roughness of 0.012–0.025 µm.
- SPI B-2 has a finish of Medium semi-gloss.
- SPI B-2 has a surface roughness of 0.10–0.15 µm.
- SPI C-3 has a surface roughness of 0.63–0.70 µm.
- Super high gloss, polished with a Grade #3 (6000-grit) diamond buff to Ra 0.012–0.025 µm.
- Medium semi-gloss, finished with 400-grit paper to Ra 0.10–0.15 µm.
- Normal matte, polished with 320-grit stone to Ra 0.63–0.70 µm.
Tolerance Reference
- The tolerance with drawing for CNC Milling is as low as +/- 0.005 mm.
- FDM 3D printing offers a low-cost component with average accuracy and uses thermoplastics for 3D printing.
- Wire Cut EDM is highly accurate.
- The U6 H.E.A.T machine achieves tight tolerances.
- Die sinker EDM is capable of maintaining tight tolerances
- The shop needs to have CNC machines that can achieve a specific tolerance.
Industries We Serve
- antennas
- automotive
- CNC machined parts
- custom parts
- electronics
- medical diagnostic
- optical displays
- optical_systems
Material Reference
- ABS
- Austenitic Stainless Steel
- Carbon steel
- ceramic
- composites
- Copper - T2
- copper or graphite
- Hardened Materials
- High Impact Polystyrene
- Low-density polyethylene
- MDF
- metal
- Polybutylene Terephthalate
- SUS304
- thermoplastics
- thick metal sheets
- tungsten carbide
Ordering, Lead Times & MOQ
Custom CNC parts carry no forced MOQ; ordering from a single prototype piece is standard industry practice.
Instant-quote platforms publicly advertise prototype lead times of 1-3 business days.
Online RFQ is the industry-standard flow: upload a 3D model (STEP/STP/DWG/DXF), receive an instant quote or engineer review, then production, inspection, and delivery.
Frequently asked questions
What is the minimum order quantity for aerospace machining?
There is no fixed MOQ. We accept single-piece prototype orders and bridge-production runs, though per-part pricing improves significantly at higher volumes. Many aerospace programs start with 1–10 first articles for qualification, then move to recurring orders of 50–500+ pieces. State your projected annual usage in the RFQ so we can quote volume pricing accurately.
How long do aerospace machined parts take to produce?
Lead times depend on complexity, material availability, and finishing requirements. Prototypes in common alloys such as 6061 aluminum typically ship within 5–15 business days. Parts requiring specialty materials, tight-tolerance inspection, or multiple finishing operations generally run 3–6 weeks. First article inspection and certification documentation add time, so build them into your schedule for flight-critical or qualification parts.
What files do I need to submit for a quote?
Provide 3D CAD files in STEP or IGES format along with 2D drawings that specify tolerances, critical dimensions, material, finish, and inspection requirements. If drawings are incomplete, our engineering team can flag ambiguities before quoting. For programs with export control restrictions such as ITAR, mention this in your RFQ so we can confirm the applicable requirements up front.
What quality documentation comes with aerospace parts?
Standard deliverables include a dimensional inspection report and material certificates traceable to the mill. On request, we provide first article inspection reports (FAI), certificates of conformance, and full material traceability. Because documentation requirements vary across aerospace programs, list the reports you need in your RFQ so quoted pricing reflects the full inspection scope.
How is my design data protected?
Design files are used only to quote and produce your parts, and NDAs can be executed before any technical data is released. Data handling follows documented practices and access is limited to the engineering personnel assigned to your project. For export-controlled designs, we confirm applicable restrictions up front.
What tolerance should I specify?
Specify tight tolerances only on critical features. Standard ±0.1 mm covers most features. Tighter tolerance = cost multiplier; apply selectively via drawing GD&T.
How is quality controlled?
First-article inspection in our own shop before the first production order. In-process checks. Final inspection report (dimensions) with shipment. Material certs (mill test reports) on request.
Is my design protected?
NDA before file exchange. Files used only for your production. No resale of custom designs.
Which material should I choose?
Function first: strength, weight, corrosion, cost. Common pairings: 6061 general, 304/316 corrosive env., PEEK medical. See materials guide pages.
Which surface finish do I need?
Anodizing for aluminum corrosion/wear/color. Passivation for stainless. Plating for conductivity/steel protection. Cosmetic vs functional distinction.
How do you ship and what terms?
DHL/FedEx/UPS express for samples and small batches. Air/sea freight for production volumes. Incoterms: EXW/FOB/DAP/DDP options.
Sources · 3
- 3erp.comIndustry peer technical page
- focusedonmachining.comUnclassified source
- bakerindustriesinc.comUnclassified source
Technical references cited for verifiability — not supplier recommendations. Browse the research library.
Related Knowledge
Capability commitments on this page are owner-confirmed (2026-09-21).